7-Inch Screen Gas Pretreatment System CH4 CO2 Monitor
-
Model: HNAG1000-2H
-
Detection: CH4, CO2
-
Detection Principle: Catalytic combustion, Infrared
-
Detection range: CH4 0–100% LEL, CO2 0–2000 ppm
Previous: No more data
Product Description
Industrial 7-Inch Screen Gas Pretreatment System for CH4 & CO2
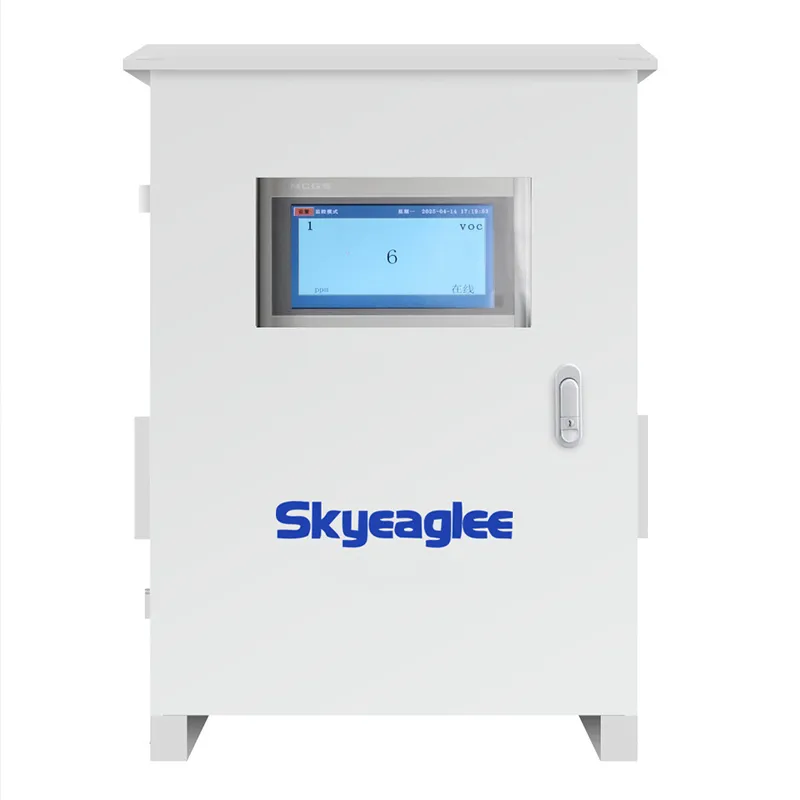
The HNAG1000-2H online gas monitoring and pretreatment system is an integrated, modular solution engineered for continuous real-time detection of Methane (CH4, 0–100% LEL) and Carbon Dioxide (CO2, 0–2000 ppm) in fixed pollution sources, flue gas stacks, and harsh industrial exhaust. Housed in a weather-resistant IP65 cold-rolled steel cabinet (with stainless steel and explosion-proof options), it ensures reliable outdoor and indoor operation.
Multi-Stage Gas Conditioning for High Temp, Humidity & Dust
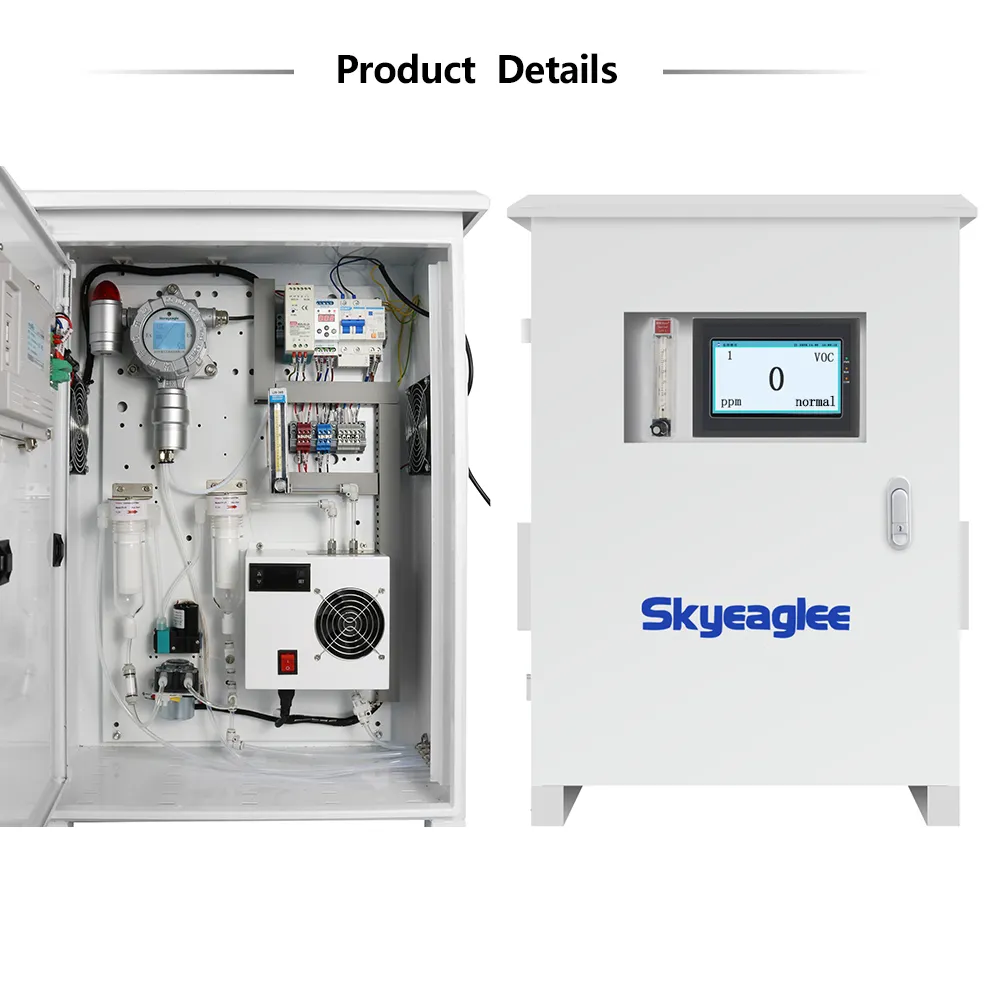
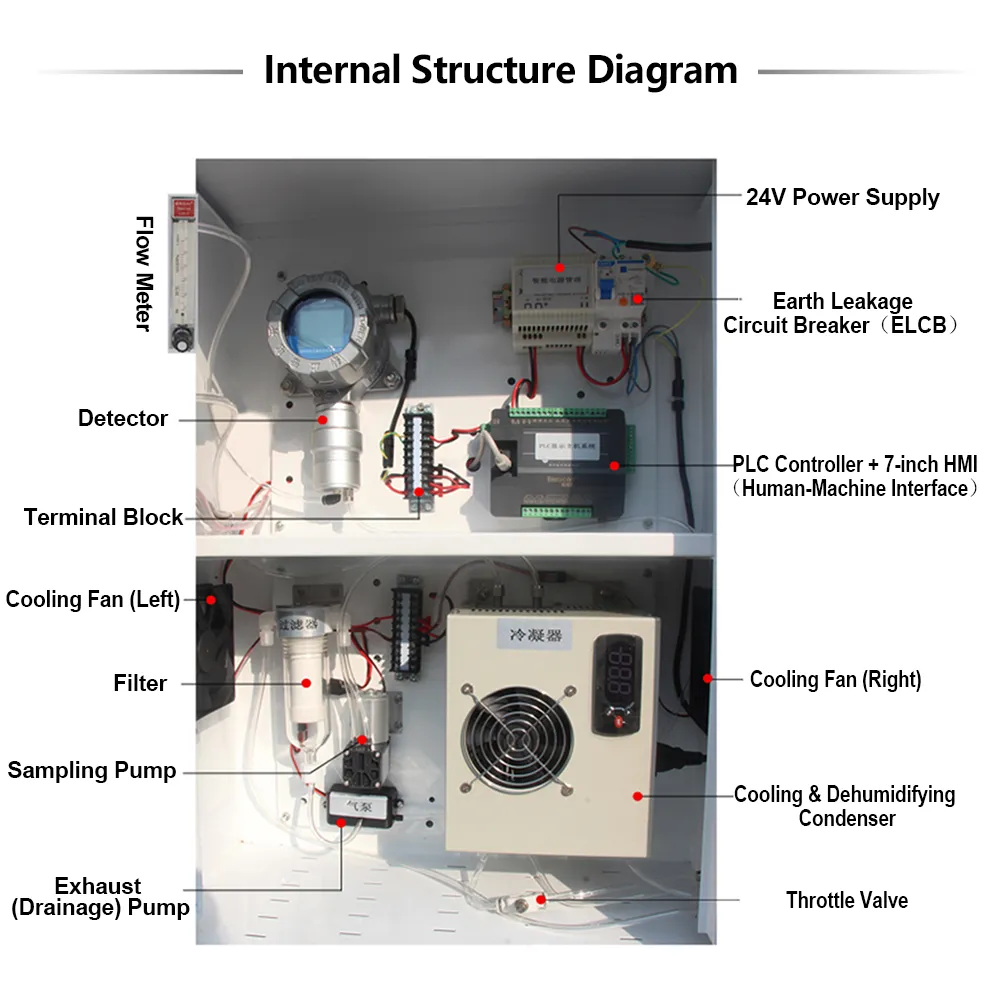
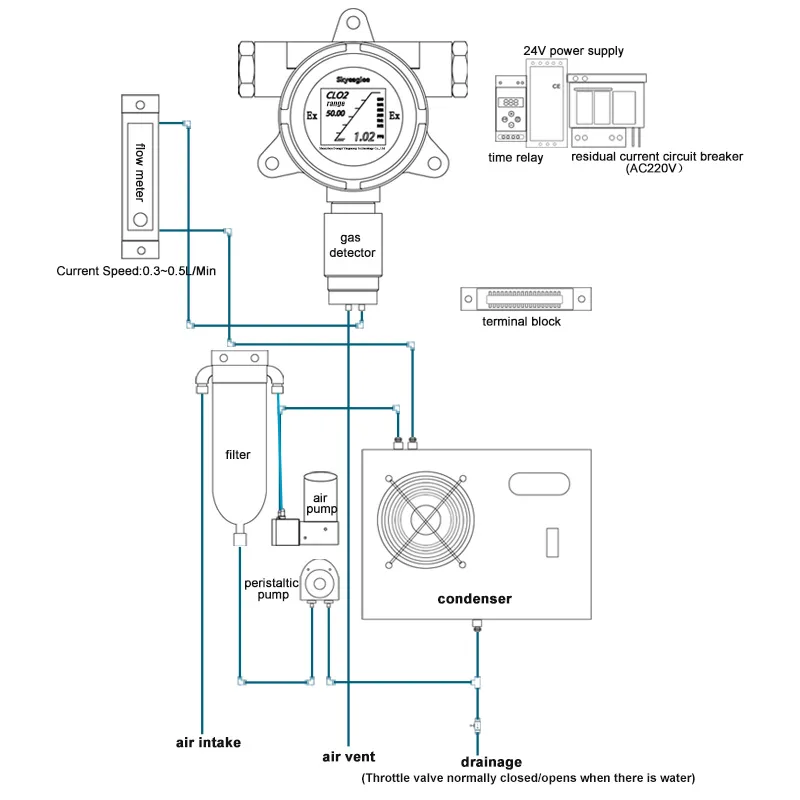
Raw industrial sample gas (-40°C to +200°C, up to 99%RH) cannot enter precision sensors directly. Our flue gas conditioning system processes the gas stream through a complete purification cycle before analysis:
Active Vacuum Sampling: A long-life vacuum sampling pump draws gas from distances of 20m (standard) up to >40m at 4 L/min.
Precision Dust Filtration: Dual high-efficiency HEPA filters remove particulate matter to prevent gas path blockage.
Cooling & Automatic Drainage: A two-stage electronic condenser lowers the gas dew point to 4°C–5°C (stabilizing output at ~25°C and 70%RH), while a peristaltic pump automatically discharges condensate water.
Catalytic Combustion & Infrared Sensor Precision
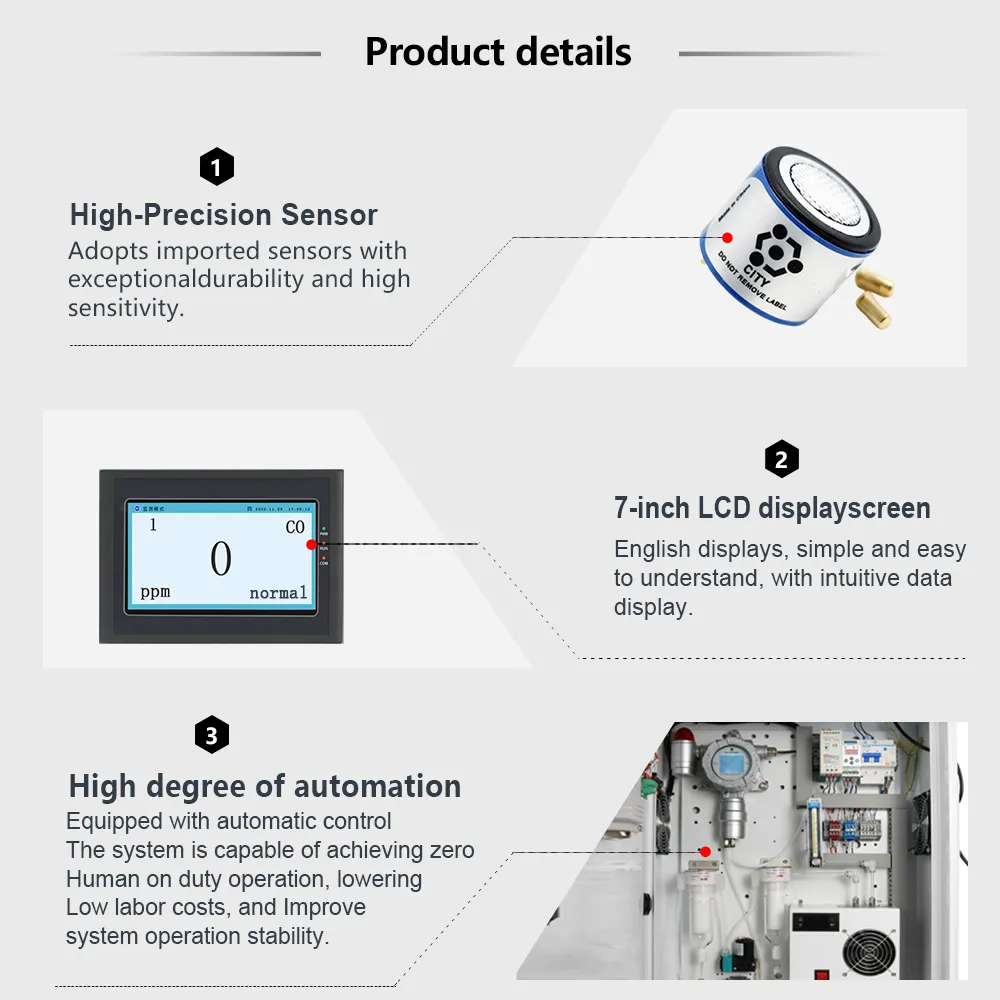
Inside the conditioned gas chamber, imported catalytic combustion (CH4) and infrared (CO2) sensors deliver rapid response times (T90≤30s), ±2%F.S accuracy, and ≤±1% repeatability. The 7-inch industrial LCD touchscreen provides intuitive English/Chinese data visualization, real-time trend curves, and massive storage for 1.8 million historical logs and 1,000 alarm records.
Smart IoT Cloud Upload & Industrial Control Integration
Built for seamless plant automation, this CH4 CO2 gas analyzer supports standalone control or integration with PLC, DCS, and DDC systems:
Standard Outputs: 12-bit 4-20mA analog signal, RS485 (MODBUS RTU protocol, 1km transmission), and passive relay switches (220VAC 3A / 24VDC 3A) to drive exhaust fans, solenoid valves, or spray systems.
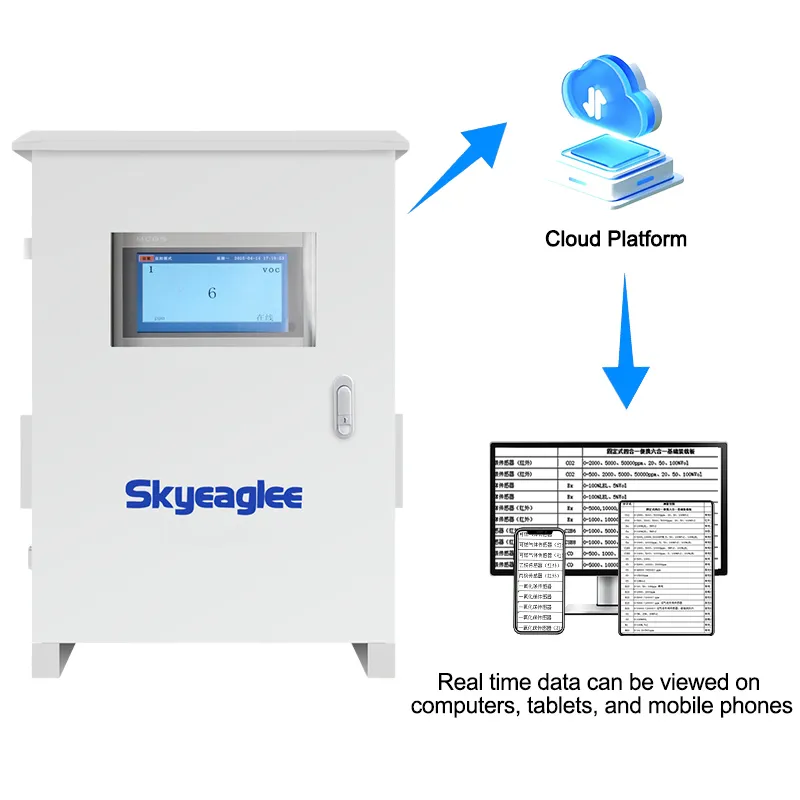
Wireless Telemetry: Optional DTU, LoRa, and HJ 212 protocol modules enable real-time data upload to Environmental Protection Bureau platforms, PCs, and mobile phones.
Customized Configurations & On-Site Applications
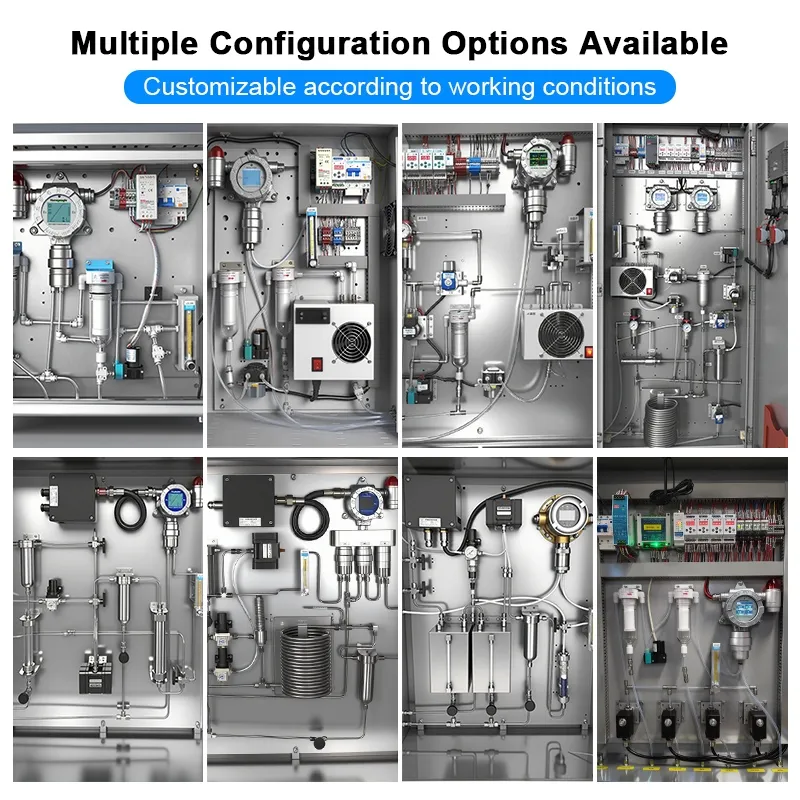
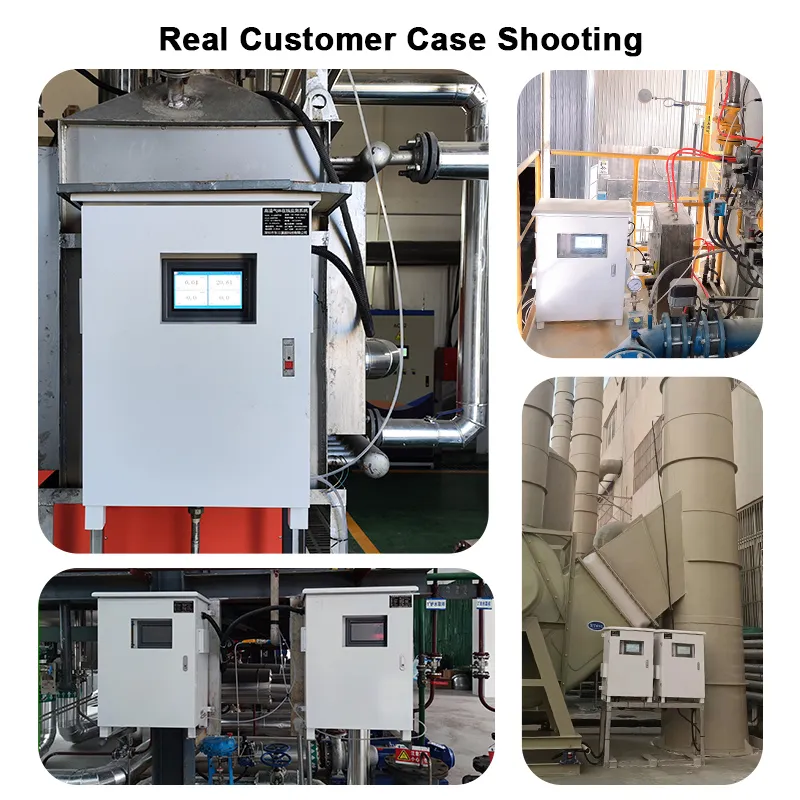
Every industrial site has unique pressure, temperature, and dust loads. We offer tailored pretreatment configurations—including pipeline heating thermostats for freezing climates, high-dust blowback devices, and oil-water separators—widely proven across petrochemical plants, thermal power stations, landfills, and wastewater treatment facilities.
Frequently Asked Questions (FAQ)
Q1: What sample gas temperature and humidity levels can this pretreatment system handle?
A1: The system is designed to sample raw flue or process gas with temperatures ranging from -40°C to +200°C and humidity up to 99%RH. Through electronic condensation and filtration, it stabilizes the sample gas to roughly 25°C and 70%RH (dew point 4°C–5°C) before it reaches the sensors.
Q2: How does the system remove condensed water automatically?
A2: After the hot, moist gas is cooled by the electronic condenser, free water is separated by the gas-water separator and continuously discharged via an integrated peristaltic drainage pump, preventing water damage to the sensors.
Q3: What is the maximum sampling distance from the flue pipe to the monitoring cabinet?
A3: The standard built-in vacuum pump supports a sampling distance of up to 20 meters. If your installation requires longer distances, an optional high-power vacuum pump can extend the sampling reach to over 40 meters.
Q4: Can the monitoring data be exported or uploaded to environmental platforms?
A4: Yes. The 7-inch touchscreen stores up to 1.8 million historical records that can be exported to Excel. Additionally, it supports 4-20mA, RS485 (MODBUS RTU), and optional wireless DTU/LoRa modules with HJ 212 protocol for direct cloud and environmental agency uploads.
Q5: What are the installation requirements and clearance space needed for the monitoring cabinet?
A5: The cabinet should be mounted vertically on a flat surface or wall (never tilted at an angle). Because it is equipped with cooling fans, ensure at least 1 meter of clear space around the unit for proper heat dissipation and do not place items on top of the enclosure.
Q6: How does the system prevent sample gas pipelines from freezing in cold outdoor regions?
A6: While the standard cabinet is IP65 waterproof for outdoor use, we offer optional pipeline heating systems with thermostats and heaters to prevent condensation from freezing inside the sampling lines in extremely cold climates.
Q7: What flow rate is required during normal operation, and how is it controlled?
A7: The standard sampling flow rate is 4 liters per minute, while the gas flow passing directly through the internal detection chamber is precisely regulated to approximately 400 ml/min using the throttle valve on the front panel flowmeter.
Q8: Can the cabinet enclosure material be customized for corrosive or hazardous explosion-proof zones?
A8: Yes. The standard cabinet is constructed from durable cold-rolled steel plate, and we provide full customization for stainless steel housings (for corrosive environments) or explosion-proof enclosures for hazardous industrial zones.
Q9: What routine maintenance is needed for the dust filters and sensors?
A9: The dual high-efficiency dust filters should be inspected and cleaned or replaced periodically to prevent particulate buildup from blocking the gas path. The internal CH4 and CO2 sensors have a typical service life of 2 to 3 years depending on the working environment.
Product Recommendation
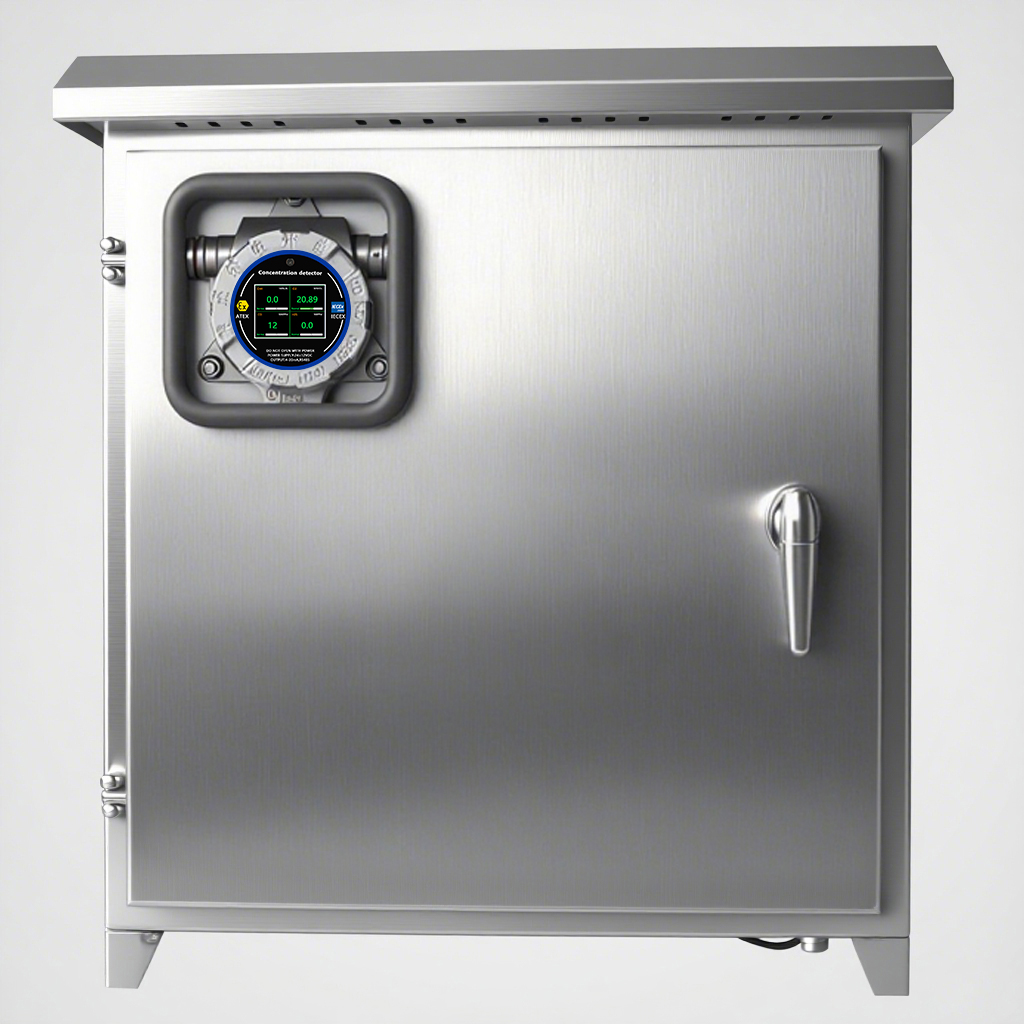
Fixed CLO2 Preprocessing Online Monitoring System-Fixed CLO2 Preprocessing Online Monitoring System
The HNAG800-CLO2 Preprocessing Online Monitoring System delivers real-time Chlorine Dioxide detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response and high accuracy within a rugged stainless steel enclosure for strict industrial safety.
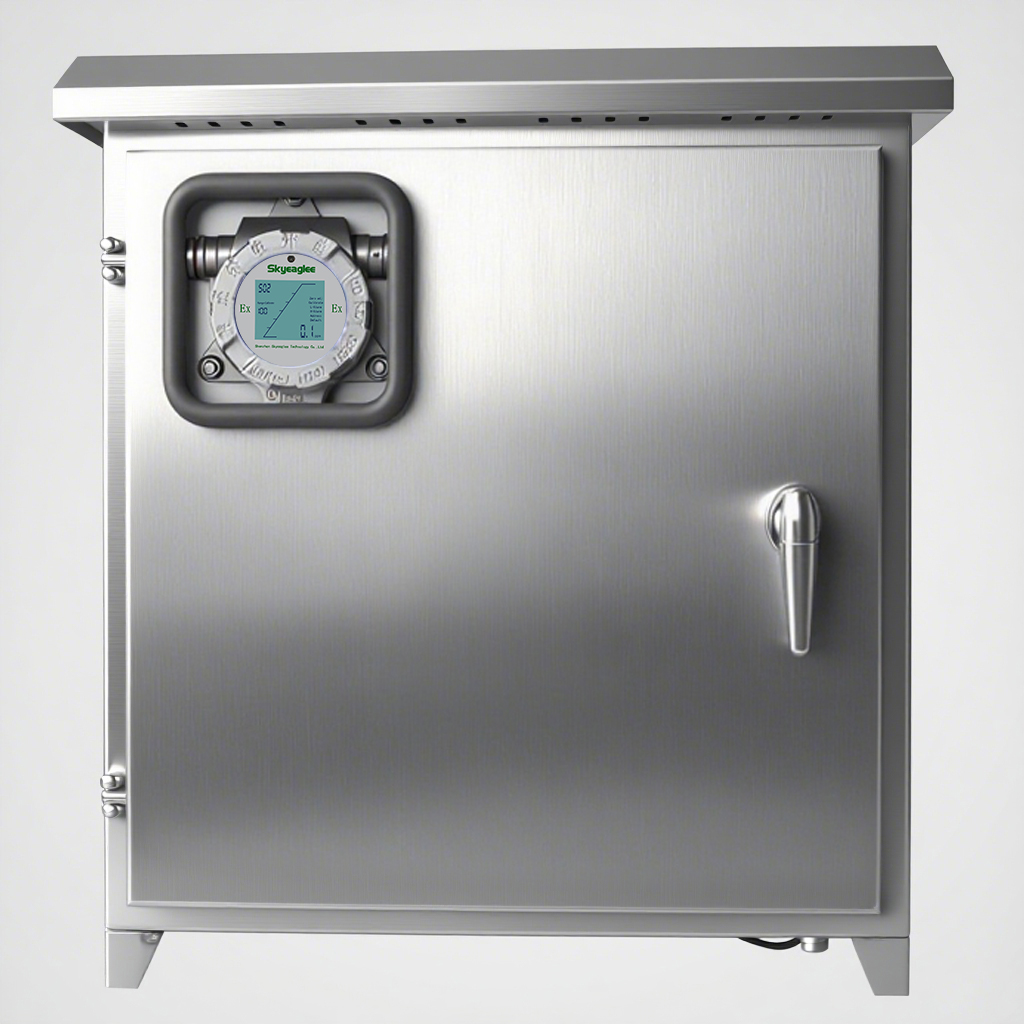
Fixed CL2 Preprocessing Online Monitoring System-Fixed CL2 Preprocessing Online Monitoring System
The HNAG800-CL2 Preprocessing Online Monitoring System delivers real-time Chlorine gas detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response and high accuracy within a rugged stainless steel enclosure for strict industrial safety.
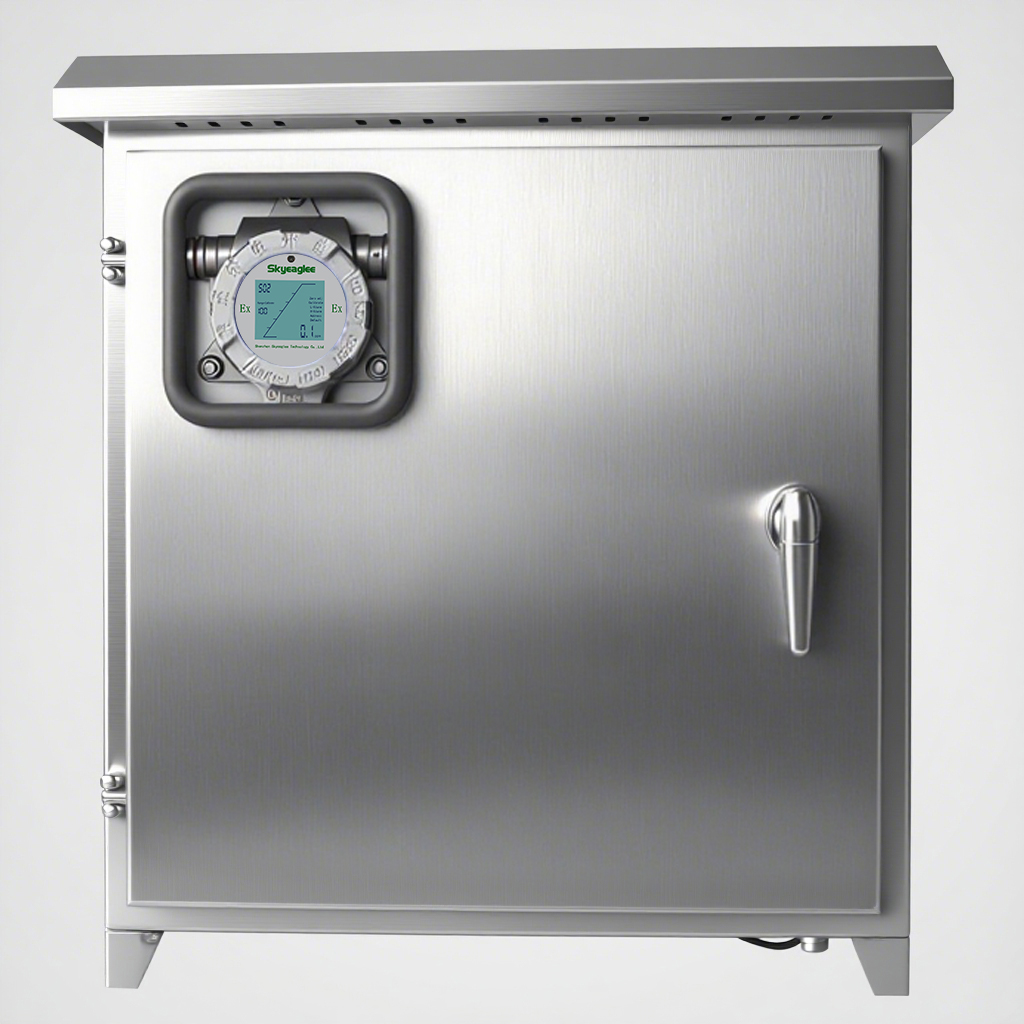
Fixed HF Preprocessing Online Monitoring System-Fixed HF Preprocessing Online Monitoring System
The HNAG800-HF Preprocessing Online Monitoring System delivers real-time Hydrogen Fluoride detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response and high accuracy within a rugged stainless steel enclosure for robust industrial safety.
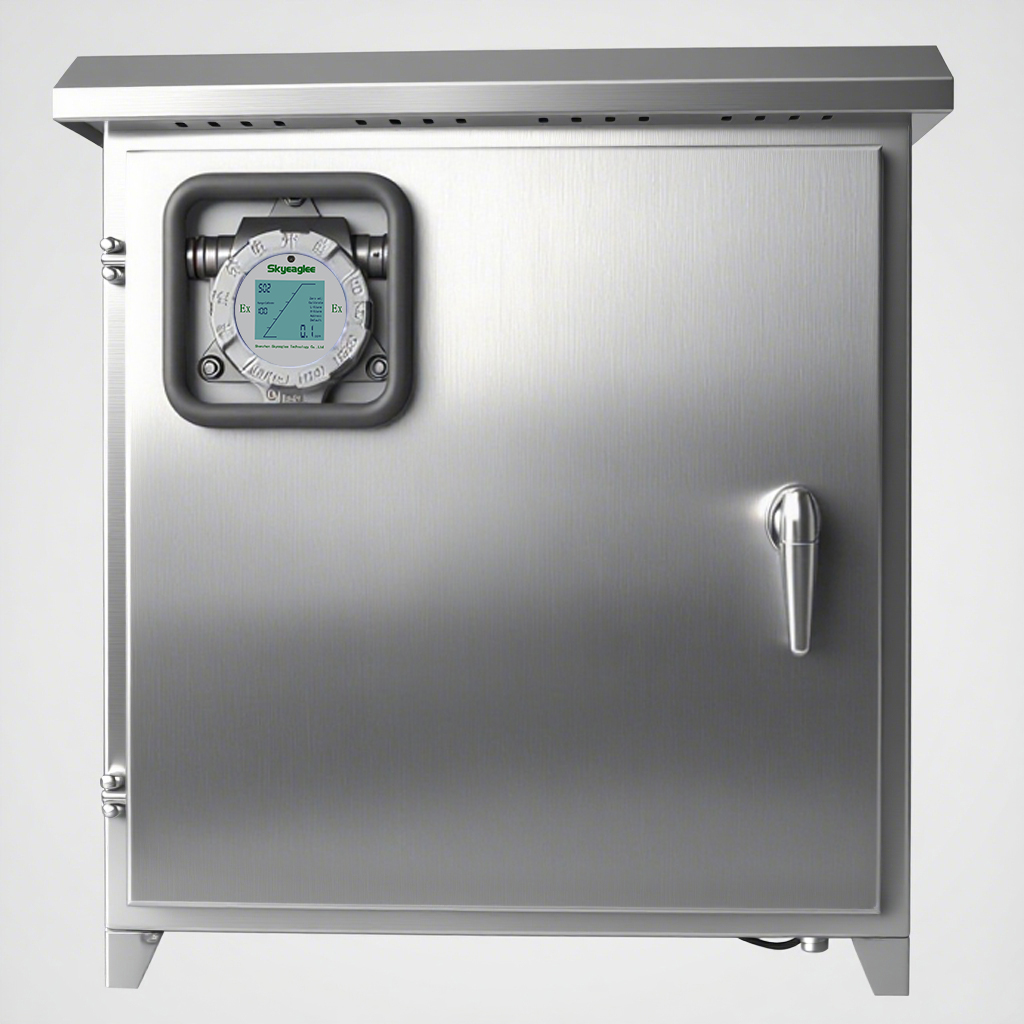
Fixed F2 Preprocessing Online Monitoring System-Fixed F2 Preprocessing Online Monitoring System
The HNAG800-F2 Preprocessing Online Monitoring System provides real-time Fluorine detection. Featuring a precise electrochemical sensor within a robust stainless steel enclosure, it ensures rapid response and high safety in harsh environments.
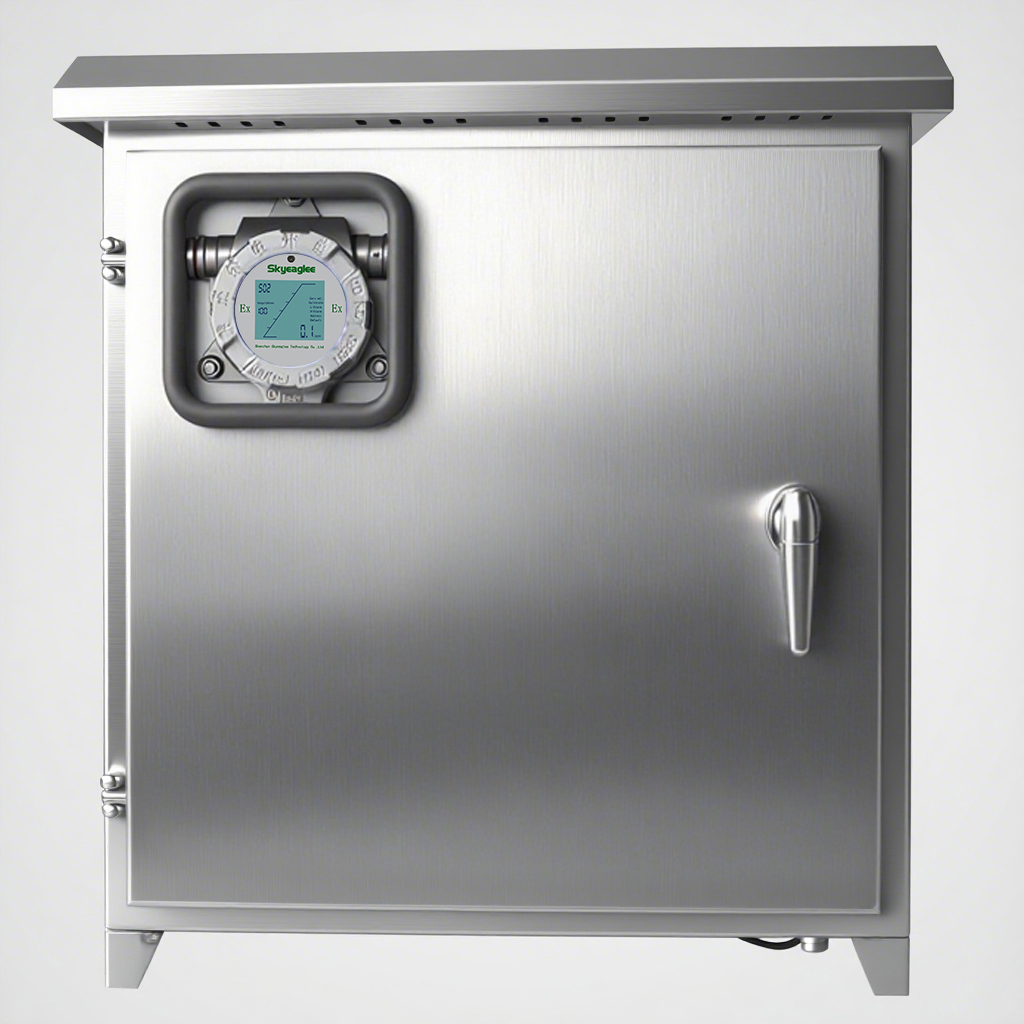
Fixed HBr/HCl Preprocessing Online Monitoring System-Fixed HBr/HCl Preprocessing Online Monitoring System
The HNAG800-HBR/HCL Preprocessing Online Monitoring System provides real-time Hydrogen Bromide and Hydrogen Chloride detection. Featuring a precise electrochemical sensor in a stainless steel enclosure, it ensures rapid response and industrial safety.
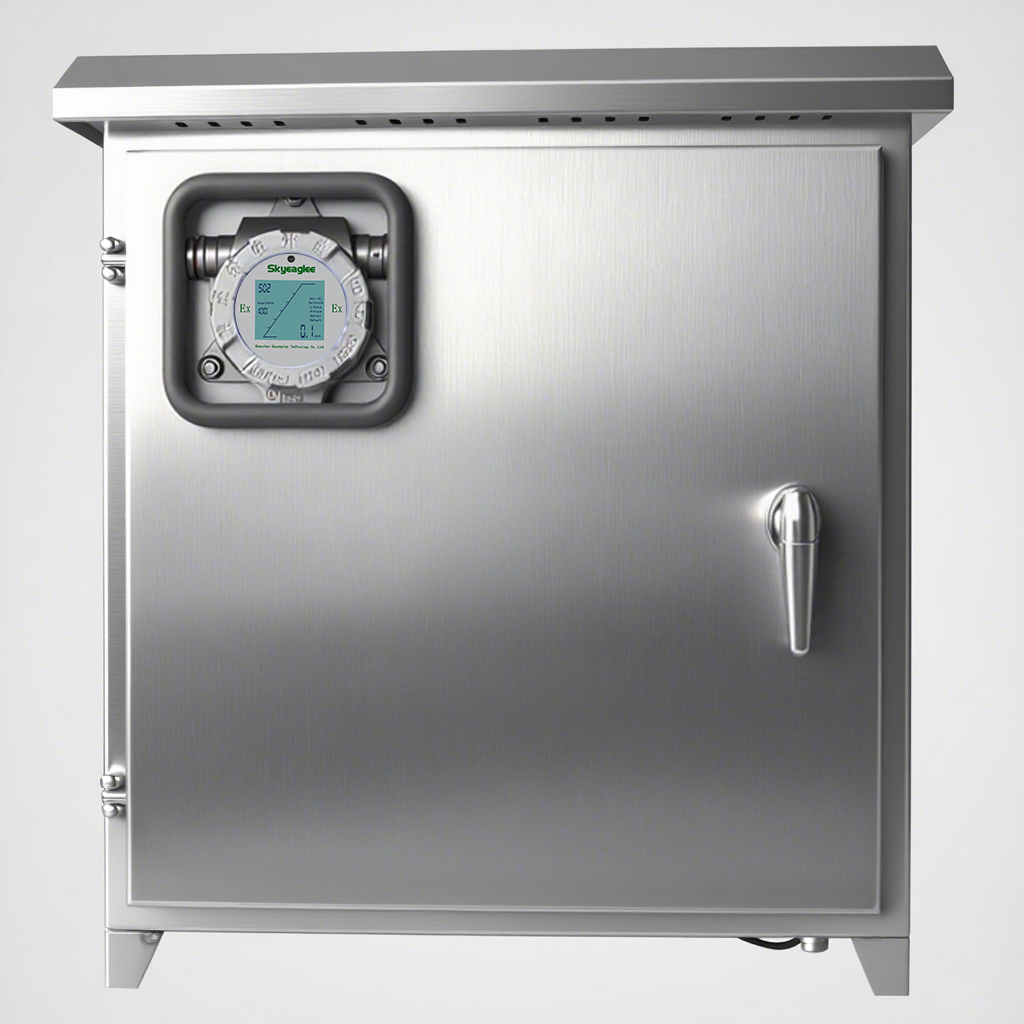
Fixed HCN Preprocessing Online Monitoring System-Fixed HCN Preprocessing Online Monitoring System
The HNAG800-HCN Preprocessing Online Monitoring System delivers real-time Hydrogen Cyanide detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response, high accuracy, and explosion-proof safety within a rugged stainless steel enclosure.
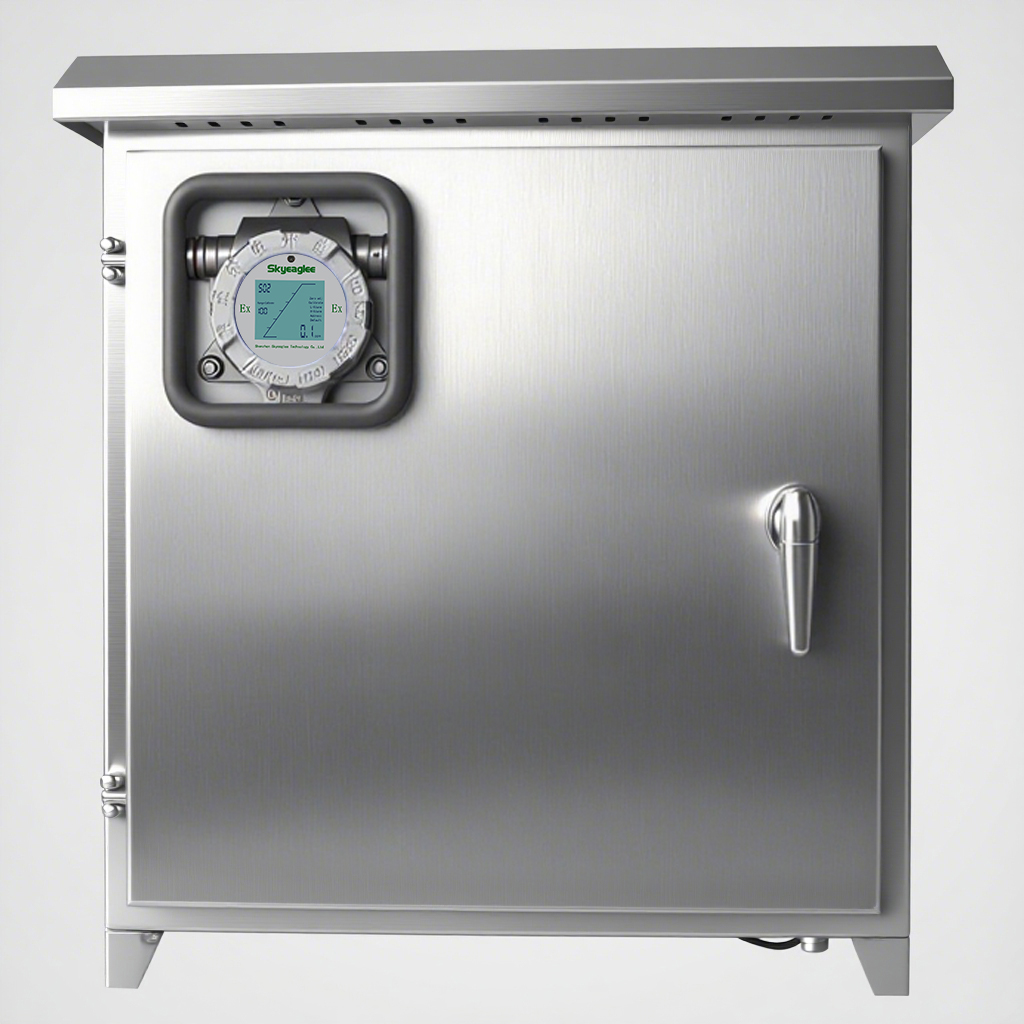
Fixed NO Preprocessing Online Monitoring System-Fixed NO Preprocessing Online Monitoring System
The HNAG800-NO Preprocessing Online Monitoring System delivers real-time Nitric Oxide detection. Featuring an advanced electrochemical sensor for atmospheric monitoring, it ensures rapid response and high precision in a rugged stainless steel enclosure.
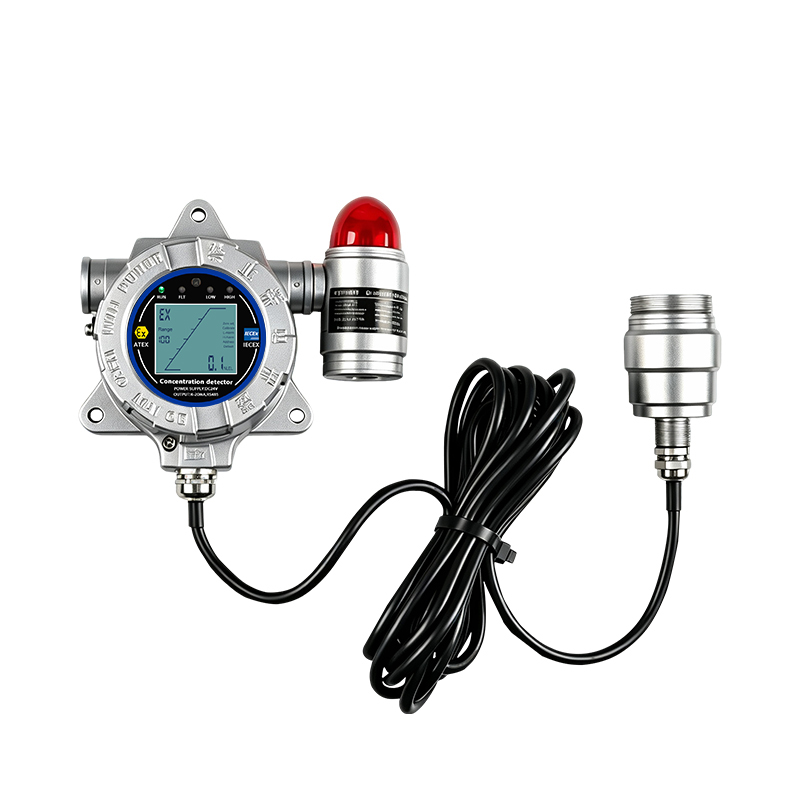
Split-Type Fixed EX Gas Detector 0-100%LEL Combustible-Split-Type Fixed EX Gas Detector 0-100%LEL Combustible
The HNAG1000-EX split-type fixed combustible gas detector monitors EX gases (0-100%LEL) in hazardous zones. Featuring a catalytic combustion sensor, remote probe, aluminum alloy housing, and 4-20mA/RS485 outputs, it ensures industrial safety.
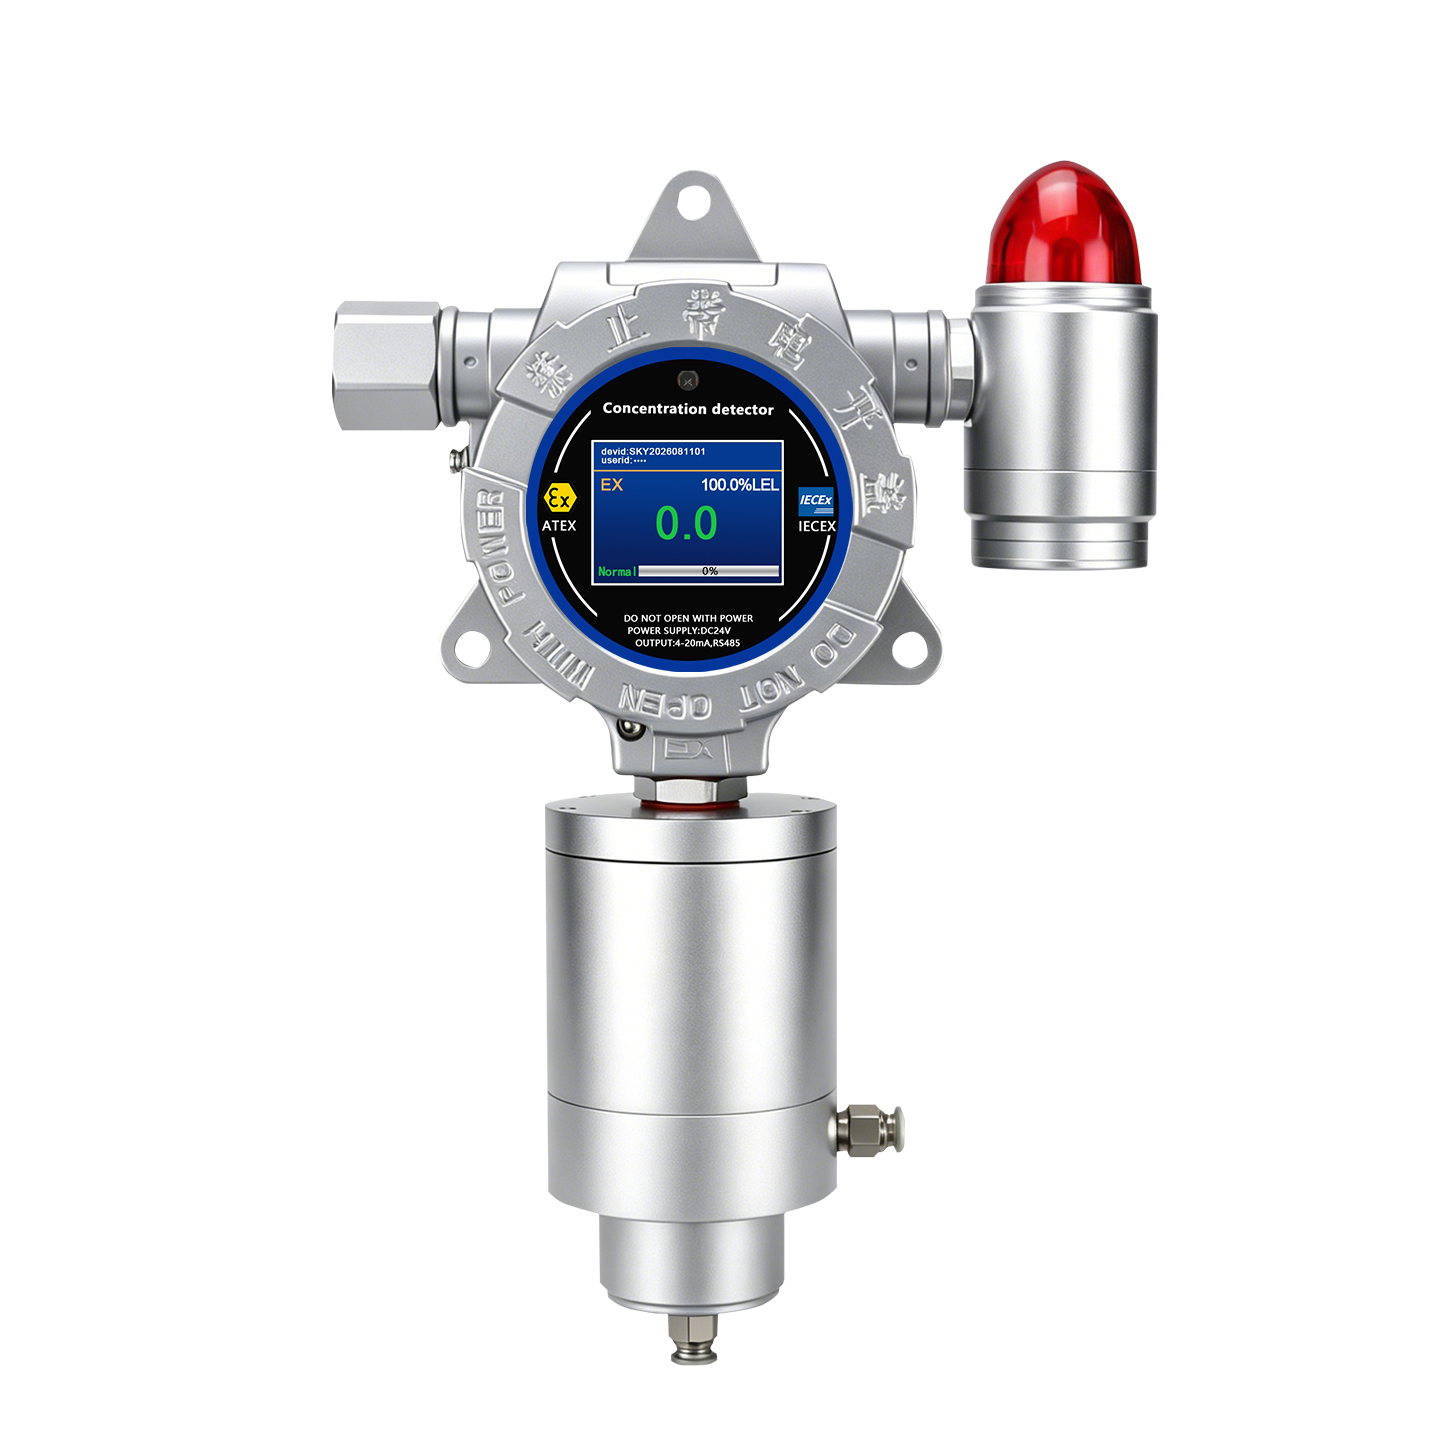
Fixed Pump-Suction O2 Gas Detector 0-1000ppm Monitor-Fixed Pump-Suction O2 Gas Detector 0-1000ppm Monitor
The HNAG1000-O2 fixed pump-suction O2 gas detector monitors trace oxygen (0-1000ppm). Built with an aluminum alloy housing, electrochemical sensor, IP66/Ex d IIC T6 ratings, and 4-20mA/RS485 outputs, it ensures continuous industrial safety.
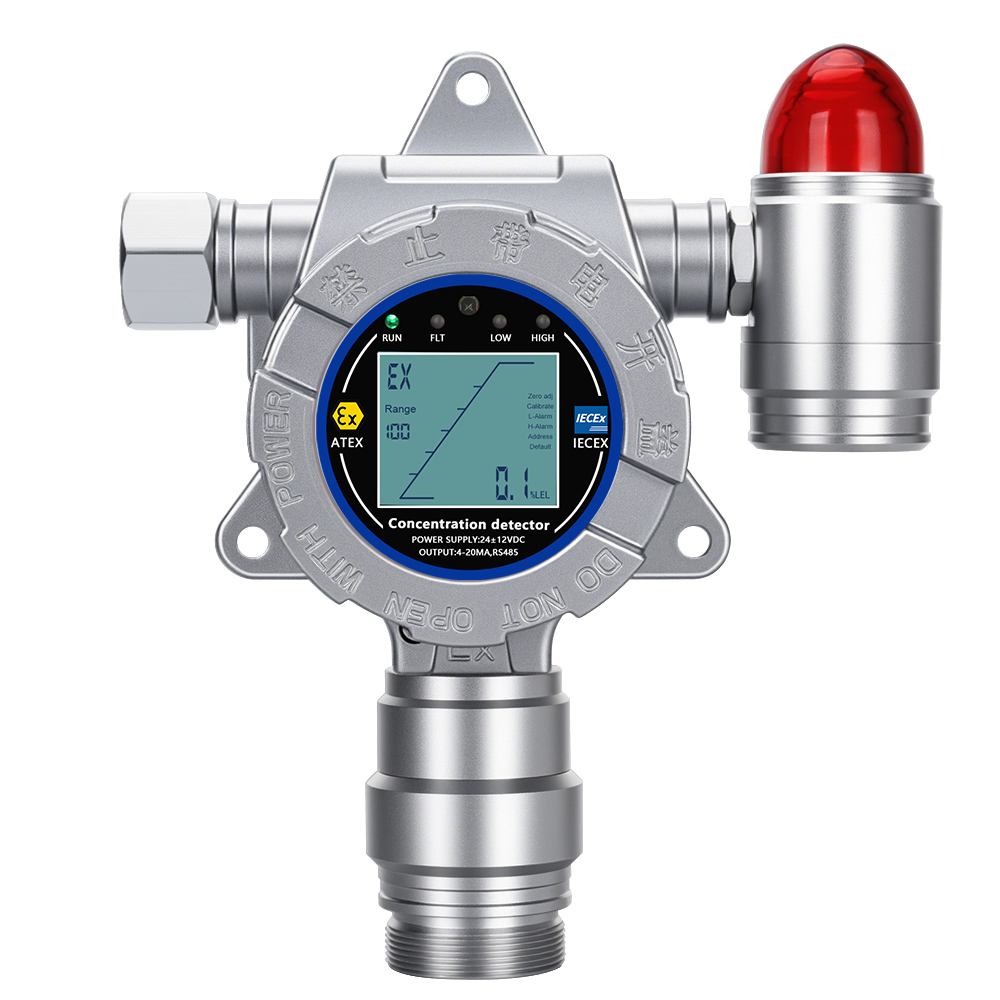
Fixed NH3 Gas Detector Ammonia Leak Monitor-Fixed NH3 Gas Detector Ammonia Leak Monitor
The HNAG1000-NH3 fixed NH3 gas detector offers real-time ammonia monitoring (0-100PPM). Featuring electrochemical sensor, explosion-proof aluminum housing, and 4-20mA/RS485 outputs.
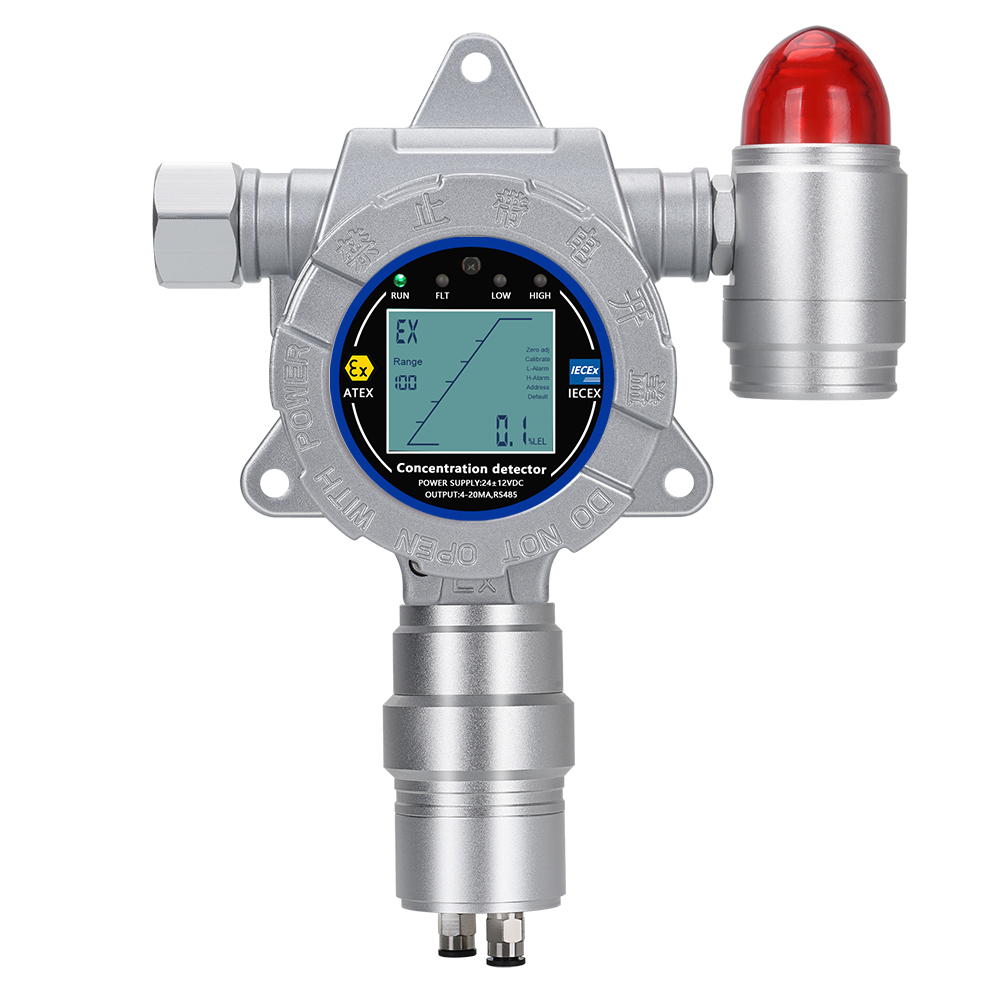
Fixed CO Gas Detector Carbon Monoxide Monitor-Fixed CO Gas Detector Carbon Monoxide Monitor
The HNAG1000-CO fixed CO gas detector ensures real-time carbon monoxide monitoring. Featuring an electrochemical sensor, explosion-proof design, and 4-20mA/RS485 outputs, it guarantees safety in industrial plants.
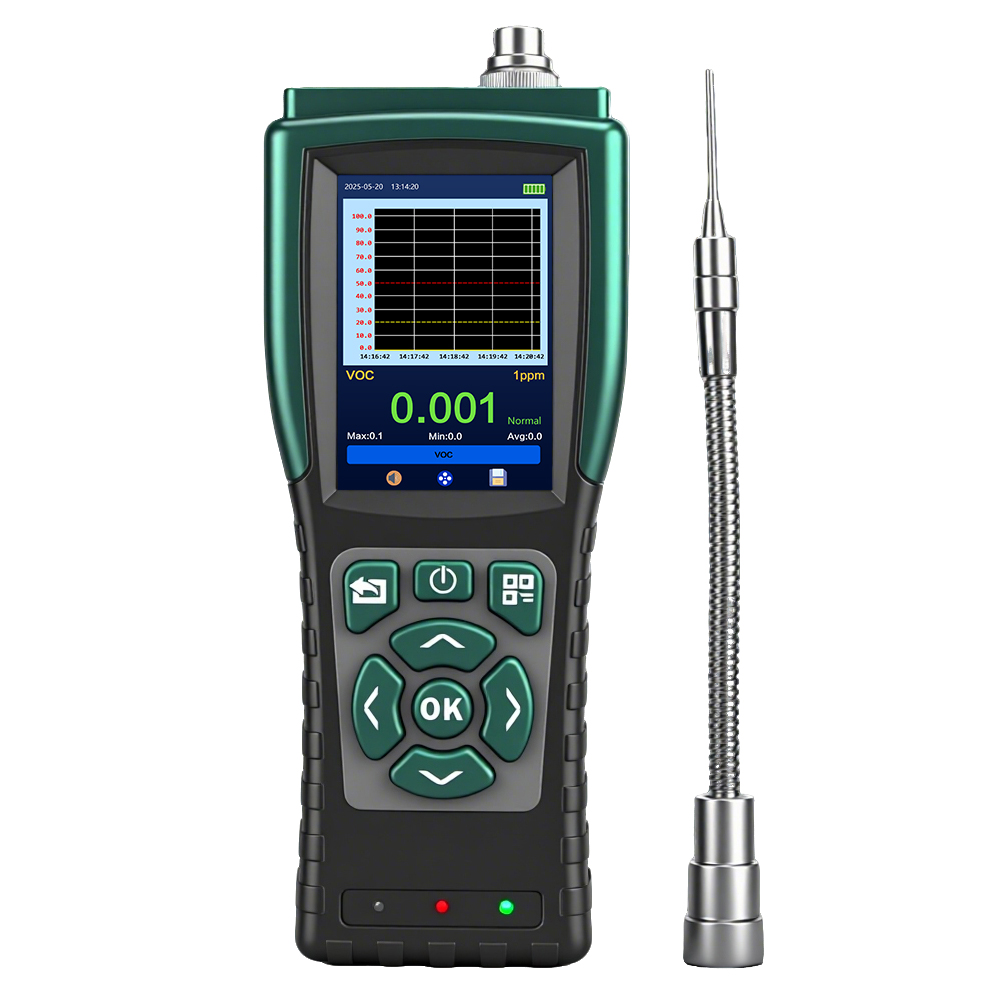
Portable VOC Gas Detector Pump Suction Monitor-Portable VOC Gas Detector Pump Suction Monitor
The HNAG900 VOC gas detector offers precise real-time monitoring of volatile organic compounds. Powered by electrochemical/PID sensors and adjustable pump suction, it features a 3.5-inch TFT screen, USB export, and Ex ib II CT4 Gb rating.
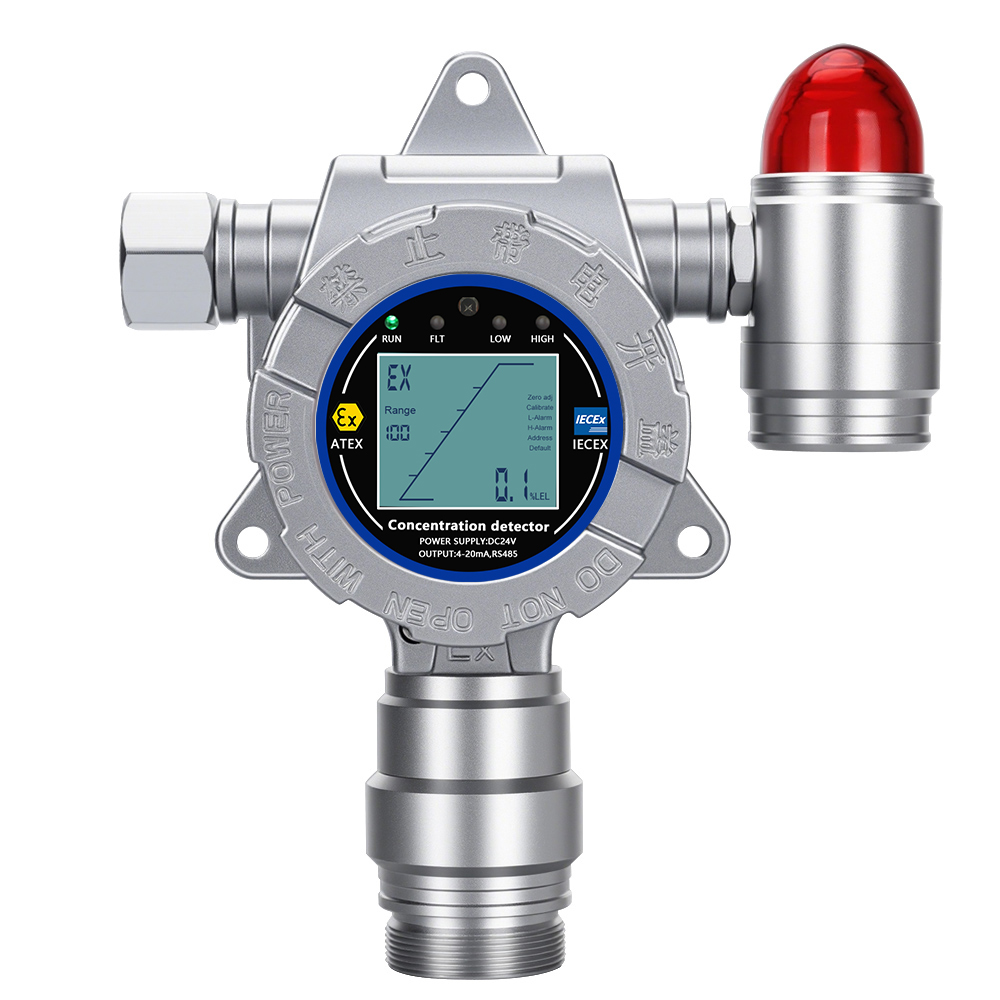
Fixed C2H4O Gas Detector: 0-100ppm Ethylene Oxide Monitor-Fixed C2H4O Gas Detector: 0-100ppm Ethylene Oxide Monitor
The fixed C2H4O gas detector (HNAG1000) provides real-time, accurate ethylene oxide monitoring (0-100 ppm). Featuring a precise electrochemical sensor, robust aluminum alloy housing, and IP66 protection, it ensures ultimate industrial safety.
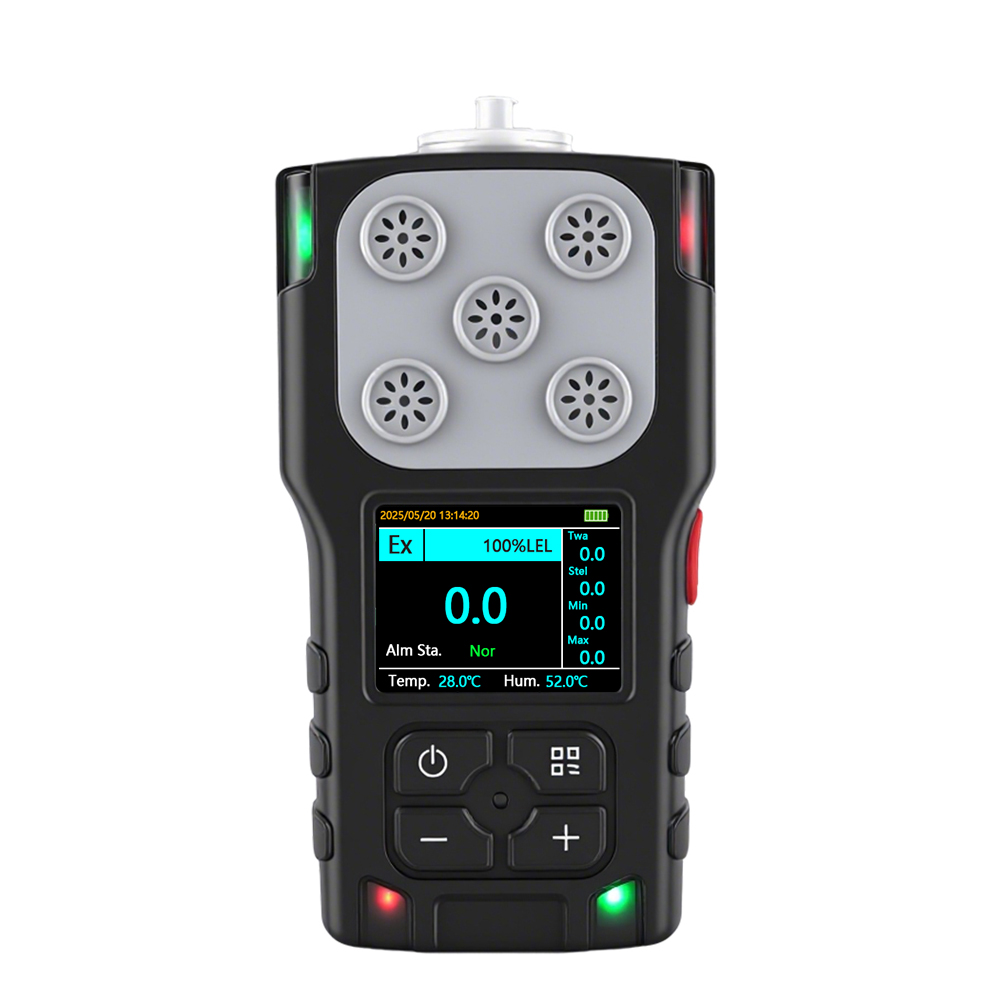
Portable H2SO4 Gas Detector Pump & Diffusion-Portable H2SO4 Gas Detector Pump & Diffusion
Portable HNAG920 H2SO4 Gas Detector offers dual pump-suction and diffusion sampling. With a precision electrochemical sensor, 2.0-inch LCD, and durable PC+TPU housing, it ensures rapid, accurate sulfuric acid monitoring for safety.
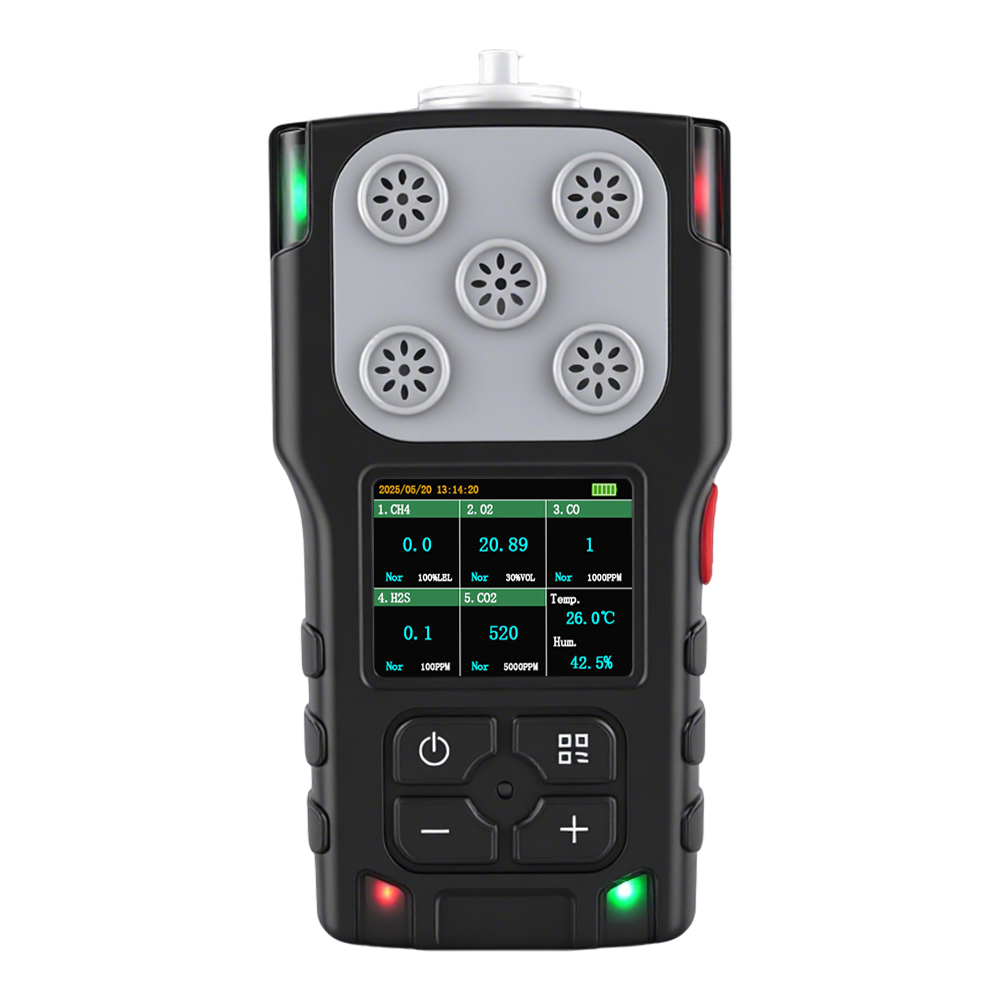
Portable Pump-Suction 3-in-1 Gas Detector-Portable Pump-Suction 3-in-1 Gas Detector
The HNAG920-3H portable 3-in-1 gas detector monitors CH4, C3H8, and H2. Featuring integrated pump-suction and diffusion modes, a 180° auto-rotating screen, and wireless transmission, it provides superior safety in complex environments.
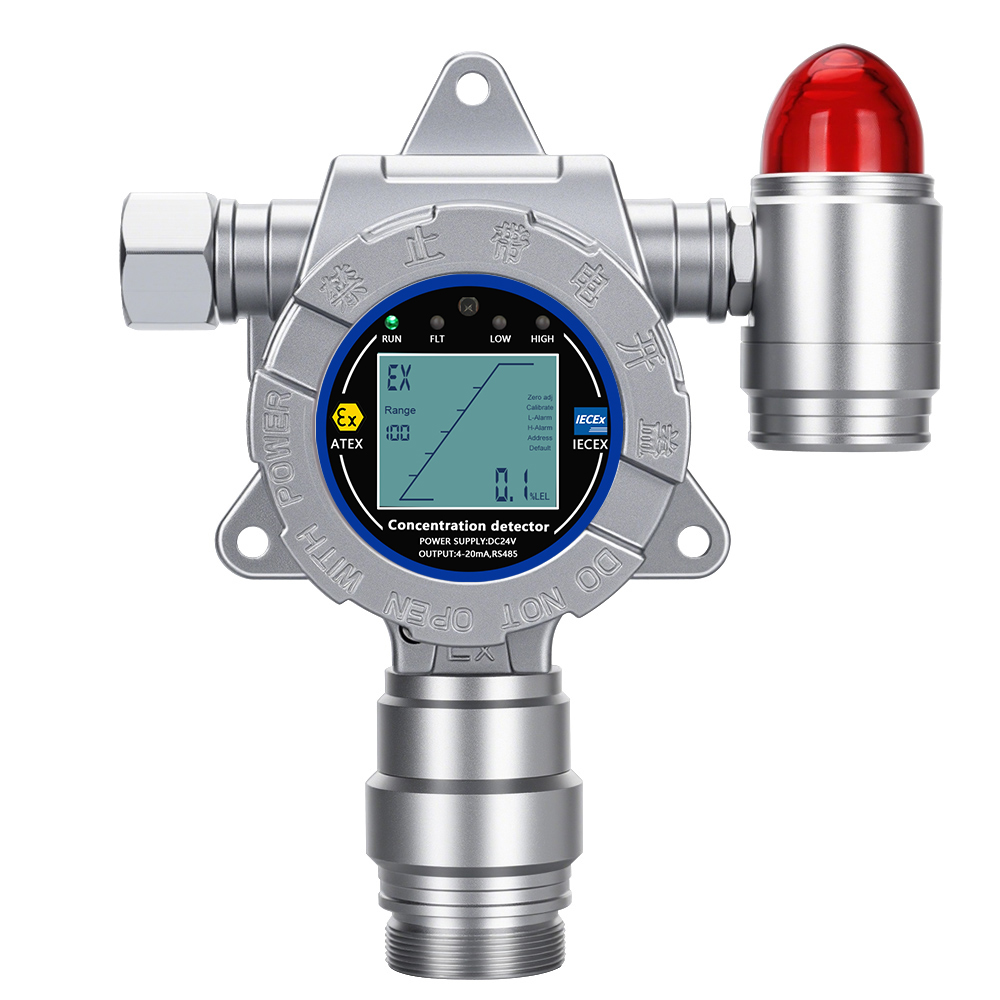
Fixed Electrochemical O3 Ozone Gas Detector-Fixed Electrochemical O3 Ozone Gas Detector
The HNAG1000-O3 fixed gas detector provides real-time, highly accurate ozone (O3) monitoring. Featuring an advanced electrochemical sensor, Ex d IIC T6 rating, and 4-20mA/RS485 outputs, it ensures maximum safety in demanding industrial environments.
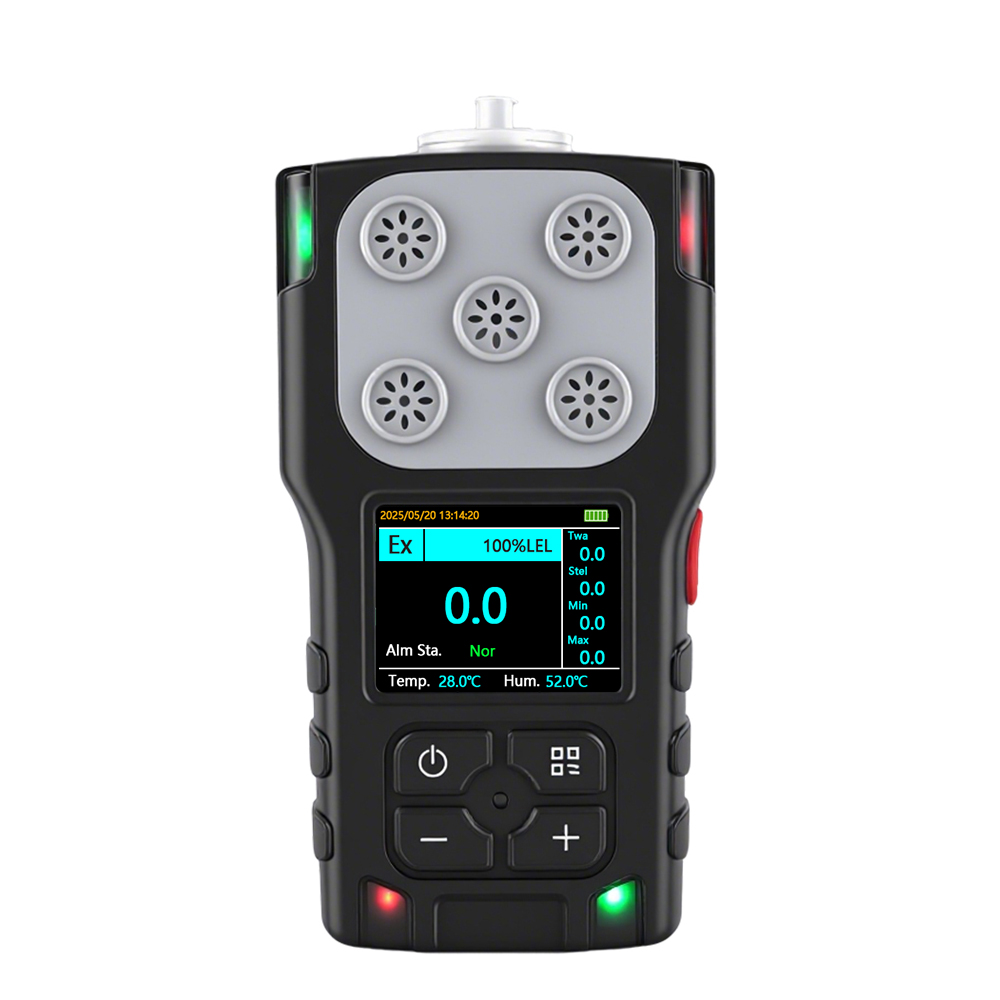
Portable Pump-Suction PH3 Gas Detector-Portable Pump-Suction PH3 Gas Detector
The HNAG920-PH3 portable gas detector offers precise real-time phosphine monitoring. Featuring a dual pump-suction and diffusion design, 2.0-inch auto-rotating screen, and wireless data export, it ensures maximum safety in hazardous environments.
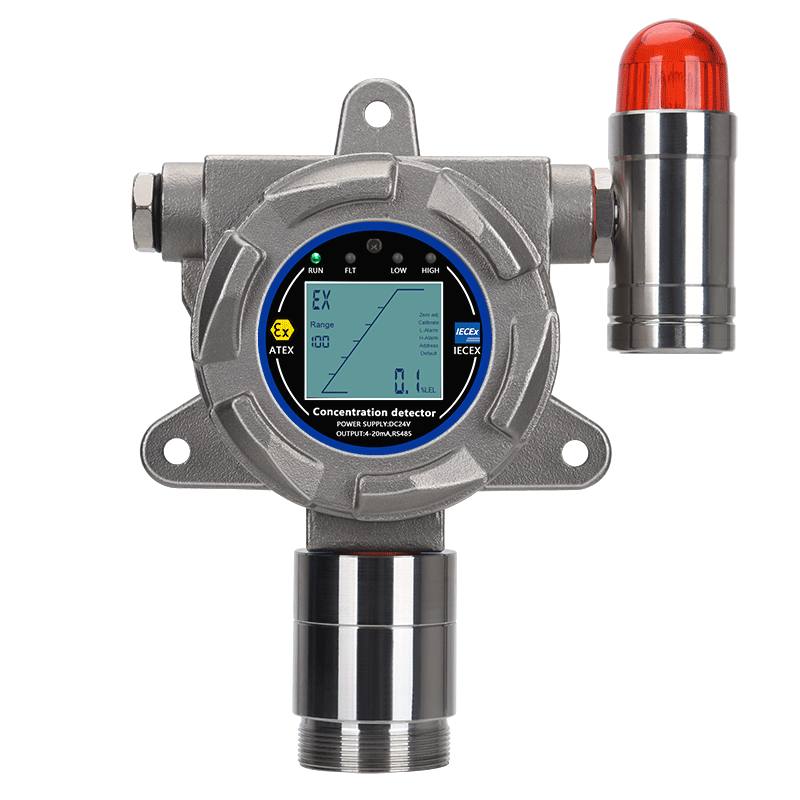
Fixed Stainless Steel H2S Gas Detector | Skyeaglee-Fixed Stainless Steel H2S Gas Detector | Skyeaglee
The HNAG1000-H2S is an industrial fixed hydrogen sulfide (H2S) gas detector featuring a rugged stainless steel enclosure. Equipped with a precise electrochemical sensor, it delivers real-time monitoring, multi-signal output, and IP66 protection.
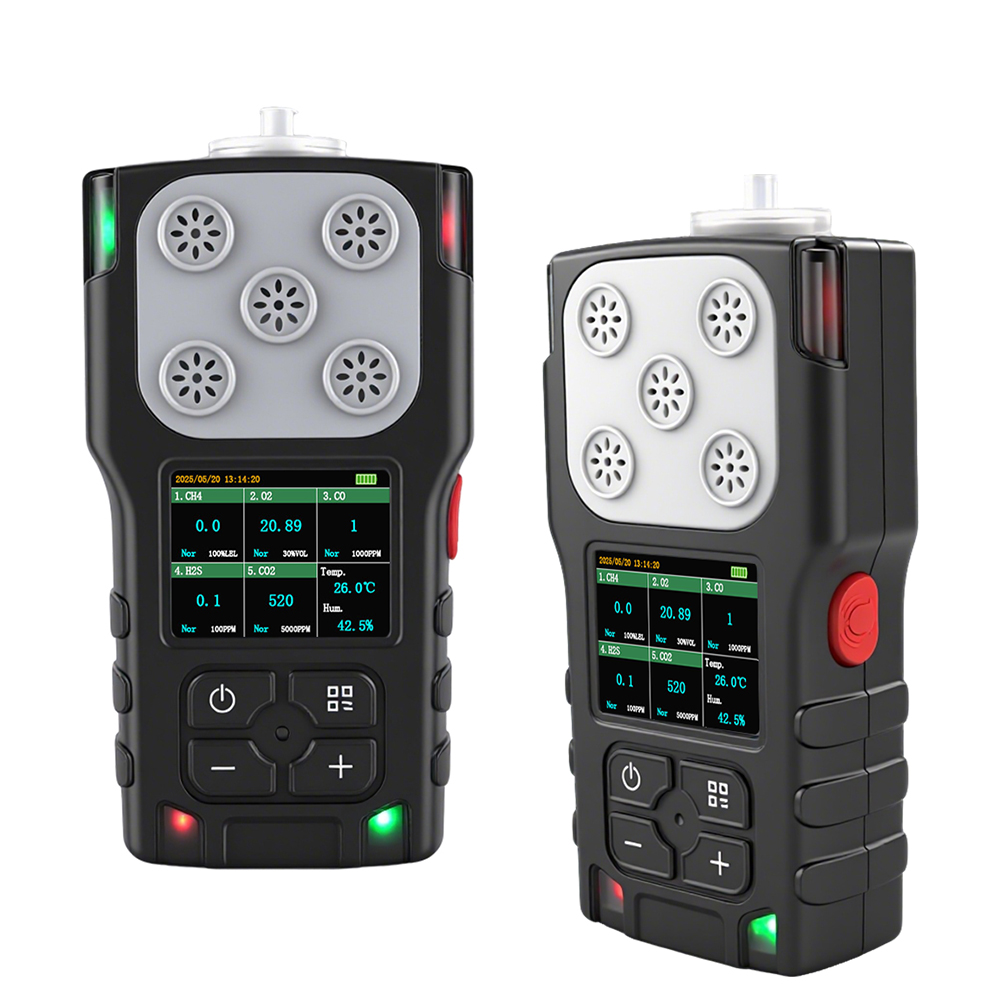
Portable 5-in-1 Pump Suction Gas Detector | Skyeaglee-Portable 5-in-1 Pump Suction Gas Detector | Skyeaglee
The HNAG920-5H portable 5-in-1 gas detector supports both pump suction and diffusion modes. It monitors O2, H2S, CO2, CO, and N2 simultaneously with high accuracy, featuring wireless transmission, a 180° auto-rotating screen, and a durable PC+TPU housing.
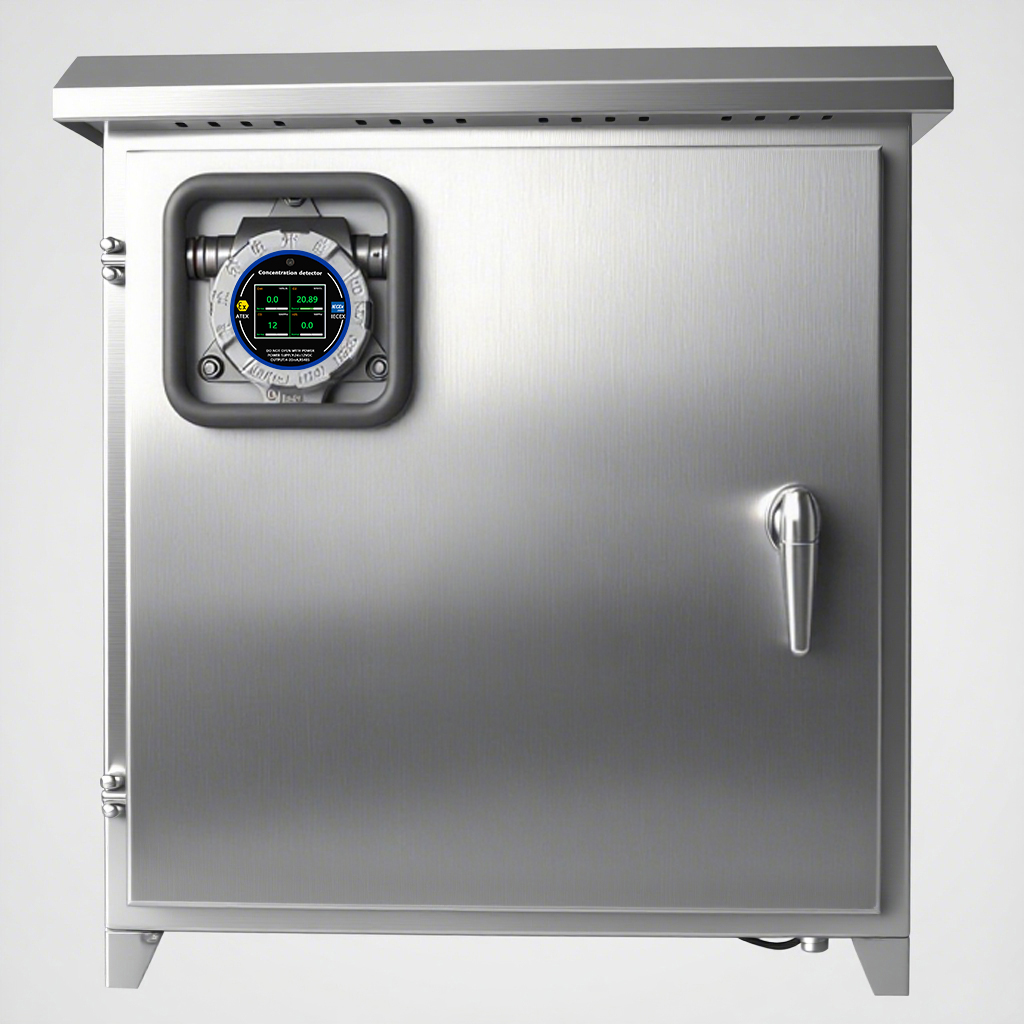
Fixed O3 Preprocessing Online Monitoring System-Fixed O3 Preprocessing Online Monitoring System
The HNAG800-O3 Preprocessing Online Monitoring System provides real-time Ozone detection. Featuring an advanced electrochemical sensor in a stainless steel enclosure, it ensures rapid response and high precision for strict industrial safety.
Fixed CLO2 Preprocessing Online Monitoring System-Fixed CLO2 Preprocessing Online Monitoring System
The HNAG800-CLO2 Preprocessing Online Monitoring System delivers real-time Chlorine Dioxide detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response and high accuracy within a rugged stainless steel enclosure for strict industrial safety.
Fixed CL2 Preprocessing Online Monitoring System-Fixed CL2 Preprocessing Online Monitoring System
The HNAG800-CL2 Preprocessing Online Monitoring System delivers real-time Chlorine gas detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response and high accuracy within a rugged stainless steel enclosure for strict industrial safety.
Fixed HF Preprocessing Online Monitoring System-Fixed HF Preprocessing Online Monitoring System
The HNAG800-HF Preprocessing Online Monitoring System delivers real-time Hydrogen Fluoride detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response and high accuracy within a rugged stainless steel enclosure for robust industrial safety.
Fixed F2 Preprocessing Online Monitoring System-Fixed F2 Preprocessing Online Monitoring System
The HNAG800-F2 Preprocessing Online Monitoring System provides real-time Fluorine detection. Featuring a precise electrochemical sensor within a robust stainless steel enclosure, it ensures rapid response and high safety in harsh environments.
Fixed HBr/HCl Preprocessing Online Monitoring System-Fixed HBr/HCl Preprocessing Online Monitoring System
The HNAG800-HBR/HCL Preprocessing Online Monitoring System provides real-time Hydrogen Bromide and Hydrogen Chloride detection. Featuring a precise electrochemical sensor in a stainless steel enclosure, it ensures rapid response and industrial safety.
Fixed HCN Preprocessing Online Monitoring System-Fixed HCN Preprocessing Online Monitoring System
The HNAG800-HCN Preprocessing Online Monitoring System delivers real-time Hydrogen Cyanide detection. Featuring a highly sensitive electrochemical sensor, it ensures rapid response, high accuracy, and explosion-proof safety within a rugged stainless steel enclosure.
Fixed NO Preprocessing Online Monitoring System-Fixed NO Preprocessing Online Monitoring System
The HNAG800-NO Preprocessing Online Monitoring System delivers real-time Nitric Oxide detection. Featuring an advanced electrochemical sensor for atmospheric monitoring, it ensures rapid response and high precision in a rugged stainless steel enclosure.
Split-Type Fixed EX Gas Detector 0-100%LEL Combustible-Split-Type Fixed EX Gas Detector 0-100%LEL Combustible
The HNAG1000-EX split-type fixed combustible gas detector monitors EX gases (0-100%LEL) in hazardous zones. Featuring a catalytic combustion sensor, remote probe, aluminum alloy housing, and 4-20mA/RS485 outputs, it ensures industrial safety.
Fixed Pump-Suction O2 Gas Detector 0-1000ppm Monitor-Fixed Pump-Suction O2 Gas Detector 0-1000ppm Monitor
The HNAG1000-O2 fixed pump-suction O2 gas detector monitors trace oxygen (0-1000ppm). Built with an aluminum alloy housing, electrochemical sensor, IP66/Ex d IIC T6 ratings, and 4-20mA/RS485 outputs, it ensures continuous industrial safety.
Fixed NH3 Gas Detector Ammonia Leak Monitor-Fixed NH3 Gas Detector Ammonia Leak Monitor
The HNAG1000-NH3 fixed NH3 gas detector offers real-time ammonia monitoring (0-100PPM). Featuring electrochemical sensor, explosion-proof aluminum housing, and 4-20mA/RS485 outputs.
Fixed CO Gas Detector Carbon Monoxide Monitor-Fixed CO Gas Detector Carbon Monoxide Monitor
The HNAG1000-CO fixed CO gas detector ensures real-time carbon monoxide monitoring. Featuring an electrochemical sensor, explosion-proof design, and 4-20mA/RS485 outputs, it guarantees safety in industrial plants.
Portable VOC Gas Detector Pump Suction Monitor-Portable VOC Gas Detector Pump Suction Monitor
The HNAG900 VOC gas detector offers precise real-time monitoring of volatile organic compounds. Powered by electrochemical/PID sensors and adjustable pump suction, it features a 3.5-inch TFT screen, USB export, and Ex ib II CT4 Gb rating.
Fixed C2H4O Gas Detector: 0-100ppm Ethylene Oxide Monitor-Fixed C2H4O Gas Detector: 0-100ppm Ethylene Oxide Monitor
The fixed C2H4O gas detector (HNAG1000) provides real-time, accurate ethylene oxide monitoring (0-100 ppm). Featuring a precise electrochemical sensor, robust aluminum alloy housing, and IP66 protection, it ensures ultimate industrial safety.
Portable H2SO4 Gas Detector Pump & Diffusion-Portable H2SO4 Gas Detector Pump & Diffusion
Portable HNAG920 H2SO4 Gas Detector offers dual pump-suction and diffusion sampling. With a precision electrochemical sensor, 2.0-inch LCD, and durable PC+TPU housing, it ensures rapid, accurate sulfuric acid monitoring for safety.
Give us a free quote
Submit this form and our sales representative will contact you soon.
Contact Us


Fill out the form