Skyeaglee SO2 Sample Gas Conditioning System
Release time:2026-09-12
Source:来源
Case Study: SO2 Continuous Emission Monitoring in Harsh Environments
The Industrial Application Scenario
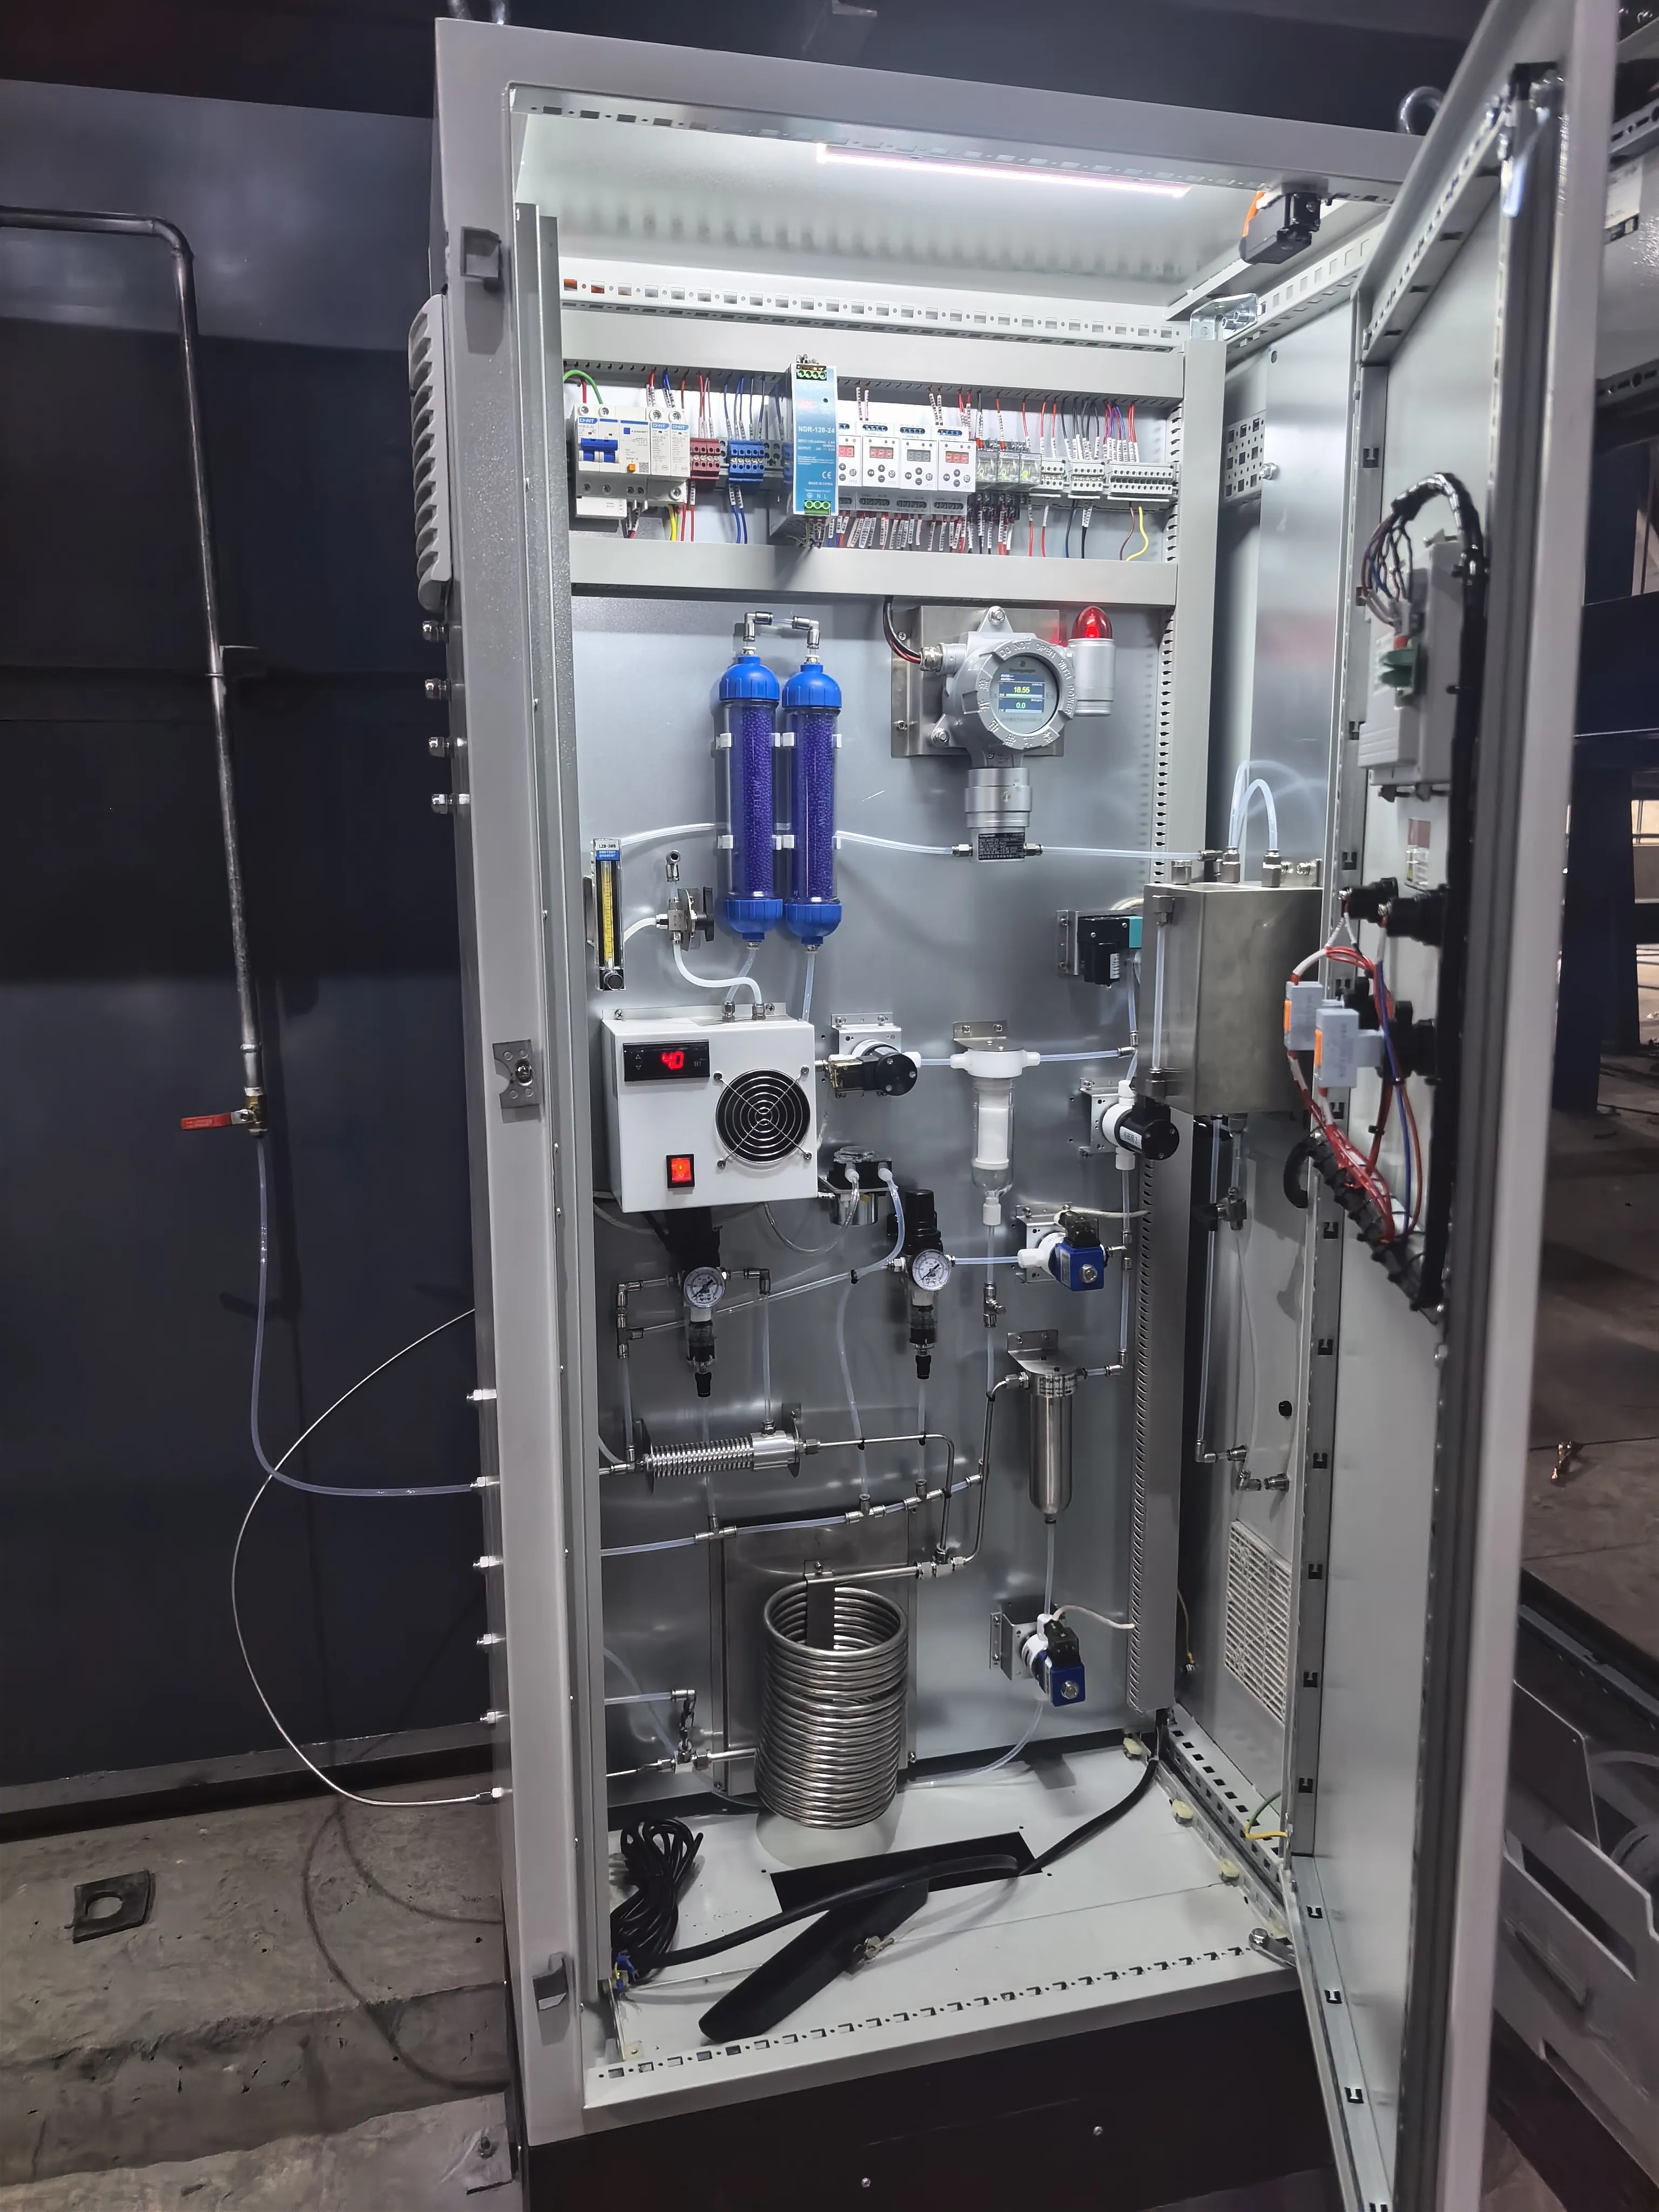
Installed directly within an industrial plant next to workshop pipelines, this Continuous Emission Monitoring Cabinet is designed for severe working conditions. Industrial exhaust gases are often extremely hot, heavily humid, and packed with particulate dust. Direct monitoring is impossible without a robust Gas Pretreatment System to extract and condition the sample gas in real time.
How the Sample Gas Conditioning System Works
To guarantee the precision of the SO2 Online Monitoring System, the internal cabinet is engineered with industrial-grade purification components. The seamless and cleanly integrated setup includes:
1.Deep Cooling and Dehumidification: Large stainless steel condensation coils rapidly drop the gas temperature and strip away excess moisture.
2.Advanced Filtration: Dual drying filter tanks (featuring blue desiccant cores) remove fine dust and residual water vapor.
3.Precision Flow and Temperature Control: Integrated flow meters and thermostatic components ensure the sample gas reaches the detector at the perfect flow rate and temperature for analysis.
Why Monitor SO2 (Sulfur Dioxide) Emissions?
Sulfur dioxide (SO2) is a highly corrosive and toxic byproduct of industrial combustion. Real-time detection of this specific gas is critical for two main reasons:
1. Ensuring Strict Environmental Compliance
SO2 is a primary contributor to acid rain and severe air pollution. By utilizing this pretreatment cabinet for accurate continuous emission monitoring, factories can prove they meet strict government environmental regulations and avoid heavy fines.
2. Protecting Infrastructure and Health
High concentrations of SO2 can corrode expensive factory pipelines and pose severe respiratory risks to on-site workers. Continuous extraction and monitoring ensure leaks or excessive emissions are caught and addressed instantly.
Case Study: SO2 Continuous Emission Monitoring in Harsh Environments
The Industrial Application Scenario
Installed directly within an industrial plant next to workshop pipelines, this Continuous Emission Monitoring Cabinet is designed for severe working conditions. Industrial exhaust gases are often extremely hot, heavily humid, and packed with particulate dust. Direct monitoring is impossible without a robust Gas Pretreatment System to extract and condition the sample gas in real time.
How the Sample Gas Conditioning System Works
To guarantee the precision of the SO2 Online Monitoring System, the internal cabinet is engineered with industrial-grade purification components. The seamless and cleanly integrated setup includes:
1.Deep Cooling and Dehumidification: Large stainless steel condensation coils rapidly drop the gas temperature and strip away excess moisture.
2.Advanced Filtration: Dual drying filter tanks (featuring blue desiccant cores) remove fine dust and residual water vapor.
3.Precision Flow and Temperature Control: Integrated flow meters and thermostatic components ensure the sample gas reaches the detector at the perfect flow rate and temperature for analysis.
Why Monitor SO2 (Sulfur Dioxide) Emissions?
Sulfur dioxide (SO2) is a highly corrosive and toxic byproduct of industrial combustion. Real-time detection of this specific gas is critical for two main reasons:
1. Ensuring Strict Environmental Compliance
SO2 is a primary contributor to acid rain and severe air pollution. By utilizing this pretreatment cabinet for accurate continuous emission monitoring, factories can prove they meet strict government environmental regulations and avoid heavy fines.
2. Protecting Infrastructure and Health
High concentrations of SO2 can corrode expensive factory pipelines and pose severe respiratory risks to on-site workers. Continuous extraction and monitoring ensure leaks or excessive emissions are caught and addressed instantly.
no data
Contact Us


Fill out the form